










How to Choose the Right Tool Coating
Selecting the perfect tool coating might seem like a nuanced art, but it’s crucial for maximizing the efficiency and lifespan of your tools. Whether you’re a seasoned machinist or new to the field, understanding the variables that impact your choice will help you make an informed decision.
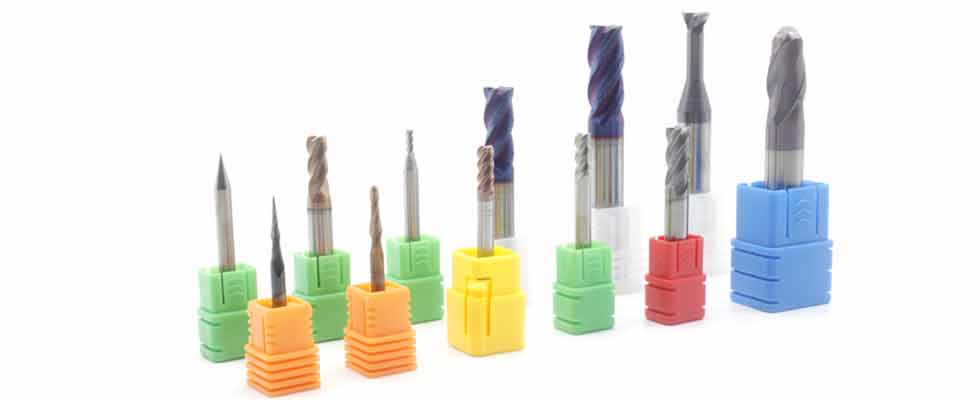
Understanding Tool Material
First things first, consider the material of the tools themselves.
- Carbide Tools
Carbide tools use a range of coating systems selected for the workpiece and operation. TiN and Diamond-like Carbon (DLC) serve different application needs; neither is a universal choice. Evaluate the complete substrate, coating, and edge geometry rather than assuming any added coating improves performance.
- High-Speed Steel (HSS) Tools
HSS tools can benefit from suitable coatings, including TiAlN in appropriate applications. The deposition process must be compatible with the HSS substrate and heat treatment. Select the system for the operation rather than assuming HSS is universally more versatile or that coating removes its temperature limits.
Understanding Traditional Coatings
Coatings such as TiN and CrN can improve surface wear behavior in suitable applications. Coating hardness does not automatically increase the toughness of the entire tool. Compare coating systems by substrate compatibility, adhesion, edge preparation, workpiece material, and service conditions.
- Titanium Nitride (TiN) Coating:
TiN can be deposited by Physical Vapor Deposition (PVD) and is used on suitable cutting and forming tools, including some HSS tools. It can improve wear behavior when the substrate and application are compatible. Its usable temperature and performance depend on the specific coating system; it does not guarantee machining quality or greater bulk tool toughness.
- Titanium Carbide (TiC) Coating:
TiC is used in cutting-tool coating systems for wear resistance. Adhesion and performance depend on the substrate, deposition process, layer architecture, and cutting conditions. Do not infer lower cutting temperature, lower forces, or suitability for all continuous cuts from the coating chemistry alone.
- Titanium Carbonitride (TiCN) Coating:
TiCN is a titanium carbonitride coating used in different coating systems and applications. Its hardness, friction behavior, and temperature capability depend on composition and deposition process. Carbon in the coating is not simply a free lubricant, and one temperature threshold cannot define the limits of all TiCN-coated tools.
- Titanium Aluminum Nitride (TiAlN/AlTiN) Coating:
TiAlN and AlTiN denote aluminum-containing titanium nitride coating families. Composition and coating architecture affect their structure, hot hardness, and oxidation behavior. A protective oxide layer may form under suitable conditions, but the as-deposited coating should not be described as simply containing an alumina thermal barrier. Select the product for the material and wet or dry cutting strategy.
- Aluminum Titanium Nitride (AlTiN) Coating:
AlTiN commonly denotes an aluminum-rich titanium aluminum nitride coating, although naming conventions vary by supplier. More aluminum alone does not guarantee better wear resistance or interruption capability. Compare the specified coating, substrate, edge preparation, and intended application.
- Chromium Nitride (CrN) Coating:
CrN coatings can provide useful wear, corrosion, and adhesion-related properties in suitable applications. Lubricant retention is not a universal consequence of a CrN grain structure. Confirm the specific product for cutting titanium, aluminum, or other materials rather than treating CrN as the preferred choice for all of them.
- Diamond Coating:
CVD diamond coatings can suit selected abrasive non-ferrous materials, graphite, and composites when the substrate and coating are compatible. Diamond is already carbon; its limitations should not be described as carbonization. Elevated-temperature chemical interaction with iron can cause rapid wear, so conventional diamond-coated tools are generally not selected for steel machining. Application limits depend on the complete tool and process.
- Cubic Boron Nitride (c-BN): Distinguish Tool Material from Coating
PCBN cutting inserts are distinct from thin c-BN coatings. The established use of PCBN grades in hard machining does not demonstrate equivalent performance for a c-BN-coated tool. Specify a verified coating product and application data before recommending it; do not present c-BN coatings as a general best choice for hardened steels, cast irons, or superalloys.
Coatings may use single-layer, multilayer, graded, or nanocomposite architectures. Their benefit depends on the complete tool and application, not the number of layers alone. Check supplier recommendations for the cutting, drilling, gear-cutting, or threading operation.
-Advantages of Tool Coating
A correctly selected coating can improve wear behavior and tool life, but an unsuitable coating can reduce performance. Confirm the benefit through comparable machining trials that include edge condition, quality, and cost per acceptable part.
-Types of Tool Coatings
Coating families include nitrides such as TiN, carbon-based systems such as Diamond-Like Carbon (DLC), and other compounds. These categories overlap with the broad term ceramic coatings. Distinguish amorphous DLC from crystalline diamond coatings and specify the actual product when comparing performance.
Application of Tool Coatings in Various Industries
Industry labels alone do not determine coating selection. Aerospace and automotive parts span different workpiece materials and operations, so begin with the actual machining requirement.
Aerospace Industry Coatings
In aerospace machining, select the coating for the particular alloy, cutting operation, substrate, and cooling strategy. TiAlN-based systems are one option in suitable applications, not a requirement for every aerospace tool.
Automotive Industry Coatings
Automotive cutting tools require coatings matched to the workpiece and operation. DLC coatings used on engine components for friction control are a different application and do not by themselves establish the best coating for the tools that manufacture those components.
Cost vs. Performance
Compare coating cost with measured tool life, cycle time, part quality, and reconditioning costs. A higher price or a superhard-material label does not establish better performance. Keep PCBN insert economics separate from claims about thin c-BN coatings.
Conclusion
Choosing the right tool coating is about balancing the type of tool, the material being machined, the machining environment, and the specific application. By considering these factors, you can greatly enhance the performance and lifespan of your tools.
FAQS
Q:What is the best coating for high-speed steel tools?
A: There is no universal best coating for HSS. Choose a deposition process and coating compatible with the tool heat treatment, workpiece, operation, and cooling conditions.
Q:Can any tool coating be used for any material?
A: No. Compatibility depends on both tool substrate and workpiece, as well as cutting conditions. Diamond coatings can suit selected abrasive non-ferrous applications, but are not a universal option for every material.
Q:How do I choose a coating for dry machining?
A: First confirm that dry machining is suitable for the tool and operation. Then use supplier recommendations for the complete substrate and coating system; TiAlN-type coatings can be candidates in appropriate applications but do not guarantee a successful dry process.
Q:What is the most cost-effective tool coating?
A: Compare cost per acceptable part under the same quality requirements. TiN may be economical in some applications, while another coating or an uncoated tool may perform better in others.
Q:Are there environmentally friendly tool coatings?
A: Environmental performance requires evidence covering deposition, service life, energy and fluid use, and end-of-life treatment. The DLC label alone does not demonstrate a lower environmental impact.