










PCD FACE MILLING
Indexable PCD Face Milling Cutters
Indexable PCD face mills for non-ferrous and non-metal faces — cast aluminum, copper, CFRP, other non-ferrous alloys and wood; ceramic-board jobs on request. Adjustable or fixed bodies, wiper options, tip heights preset before delivery (≤ 0.01 mm total tip-height difference), and adaptations of established designs to your spindle interface and fixture.
SUNDI indexable PCD face milling cutters are adjustable or fixed face-mill bodies with PCD inserts or cartridges for non-ferrous and selected non-metal faces (cast aluminum, copper, CFRP, wood; ceramic board on request). Tip heights are preset before delivery to ≤ 0.01 mm total tip-height difference.
Cast aluminum machining references
*Separate cast-aluminum references, not a combined guarantee. Final parameters depend on alloy, cutter diameter, spindle and fixture.
Common Machining Challenges — Our Solutions
- Surface finish without giving up outputMatch PCD cutting edges and wiper layout to the aluminum grade and finish target. Tip heights are preset before delivery, so you start from a controlled face instead of a long tip-setting session on the machine.
- Setup and fixture constraintsWe adapt established cutter designs to your spindle interface and fixture limits from your drawing — diameter, mounting and cartridge layout as required.
- Keep the body, replace the wear partsCompatible replacement inserts and cartridges for common tooling systems. Once part numbers and mounting dimensions match, retain the cutter body or toolholder and replace only what wears.
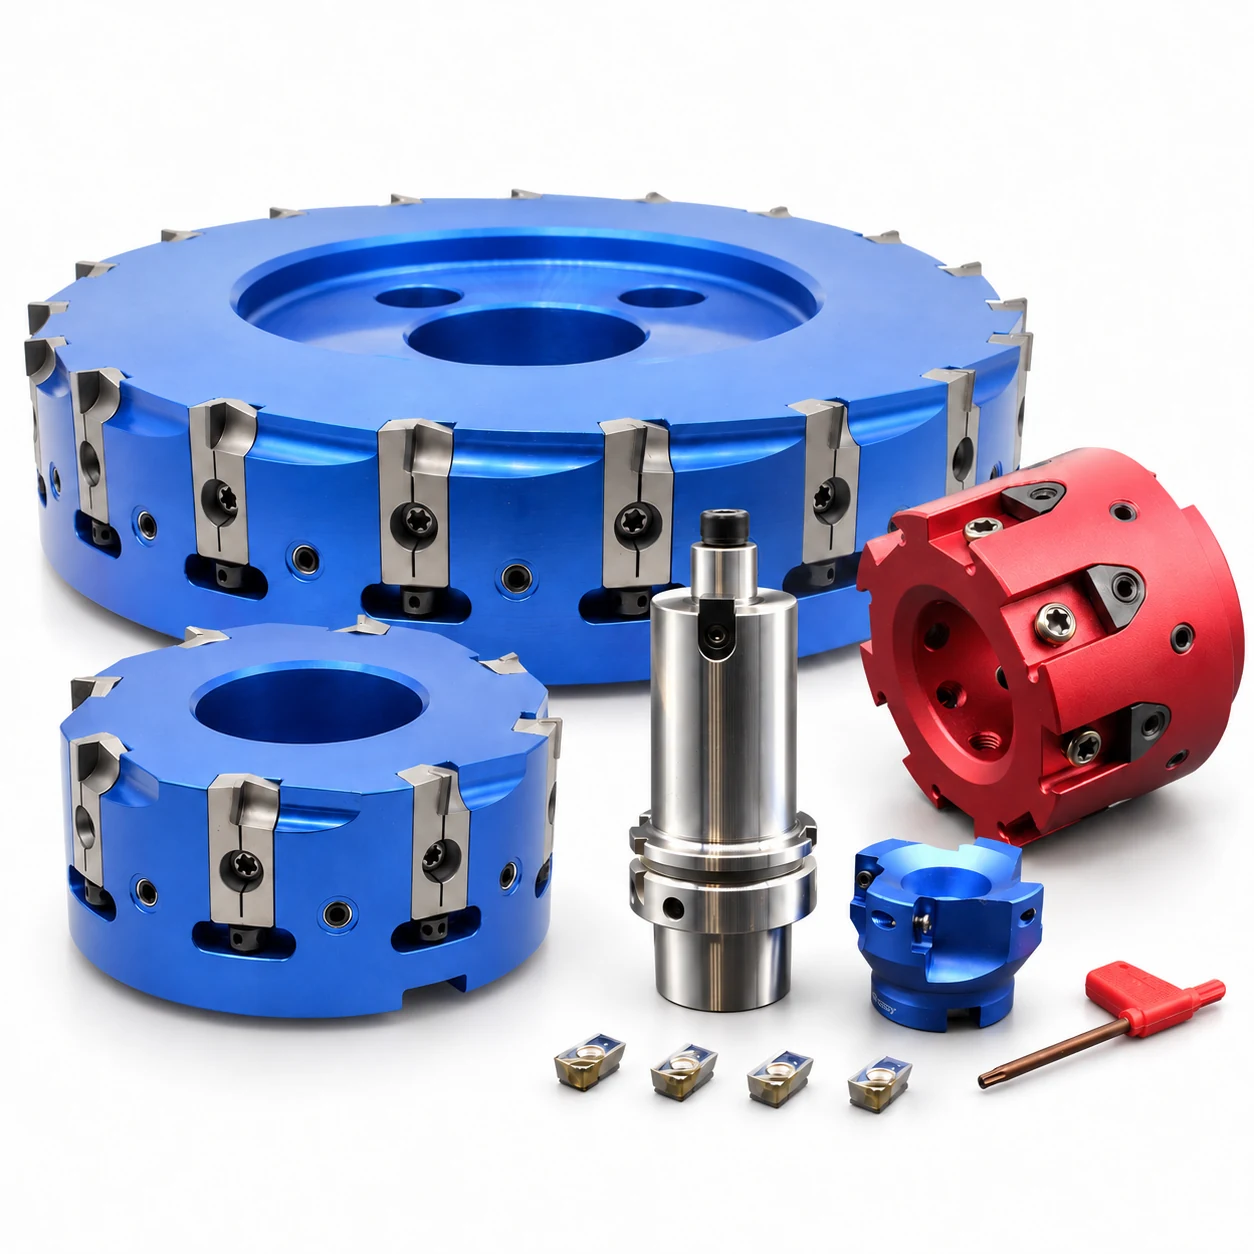
- Non-Ferrous & Composite Milling
- Wiper Options
- Preset Before Delivery
- Standard & Adapted Designs
AT DELIVERY
What Is Set Before the Cutter Ships
Before delivery, SUNDI presets cutting-tip heights so the total tip-height difference is ≤ 0.01 mm. This is a tool-setting measure, not a workpiece flatness tolerance.
Tip Heights Preset
Total cutting-tip height difference after presetting. Measured on the tool before shipment.
Edge Layout Confirmed
Wiper / cutting-edge arrangement matched to the finish target on the order (cast aluminum and other agreed jobs).
Body & Cartridge Fit
Spindle interface, cartridge and mounting dimensions confirmed from your drawing or standard catalogue body.
Cast aluminum starting Vc / fz / ap: Cutting Data Table A (after Application). Copper, CFRP, wood, ceramic board and other non-ferrous: Table B notes.
DESIGN & ADVANTAGES
Inside the Design: Six Practical Advantages
Coolant path, tip-height control, wiper edges and mounting details that decide finish, setup time and how long the head stays on the spindle.
Internal Coolant Screw & Face Outlets
Internal coolant screws and face outlets feed the cutting zone. Specify through-coolant or external supply when you RFQ so we match the cutter to your machine.
Custom Cartridges
Cartridges built to your mounting dimensions and insert layout, so the head fits the system you already run. Send the existing model or drawing with the RFQ.
Adjustment Screws
Adjustment screws set cutting-tip heights before delivery. We hold total tip-height difference to ≤ 0.01 mm — a tool-setting measure, not workpiece flatness.
Wiper Edge for Surface Finishing
Wiper options for cast-aluminum face finish. Choose the edge layout with alloy, feed and whether Ra or flatness drives the pass.
Ra 0.1 μm — cast aluminum reference with wiper setup; confirm measuring conditions on order.
Expandable Mounting Structure
Expandable mounting structure for more secure clamping on the cutter body. Ask us which series include this feature when you RFQ.
Threaded Inserts & Dynamic Balancing
Threaded inserts support repeated insert changes. Dynamic-balance adjustment is available on applicable bodies — ask for the balance condition on the diameter you run.
Ready for a Preset PCD Face Mill on Your Spindle?
Share the alloy, drawing and interface — tip-height preset and configuration confirmed before delivery. Uploads stay confidential.
PRODUCT RANGE
Choose Your PCD Face Milling Cutter
Adjustable MSF heads and fixed MFX bodies. Open each card for dimensions and ordering. Selected standard sizes may ship from stock; other configurations are made to order.
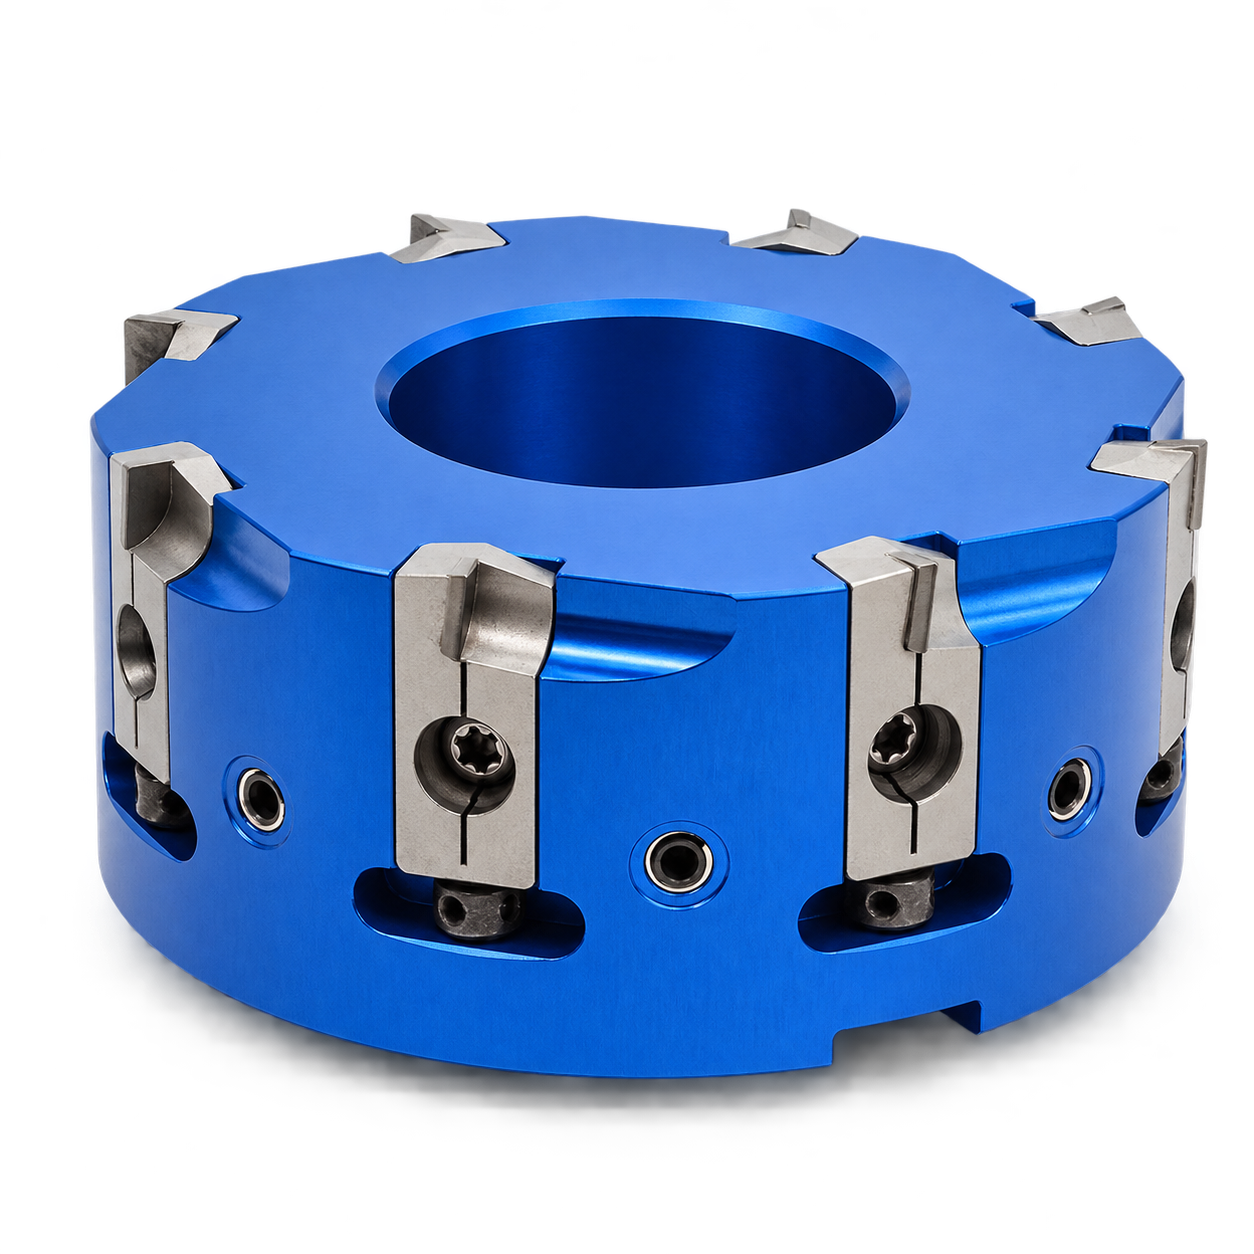
MSF-S — Coarse-Pitch Adjustable PCD Face Milling Head
Coarse-pitch adjustable heads with wider tooth spacing and wiper options. Available in Ø63–250 mm. Both MSF-S and MSF-D support wiper configurations; the series differ in tooth density.
View Details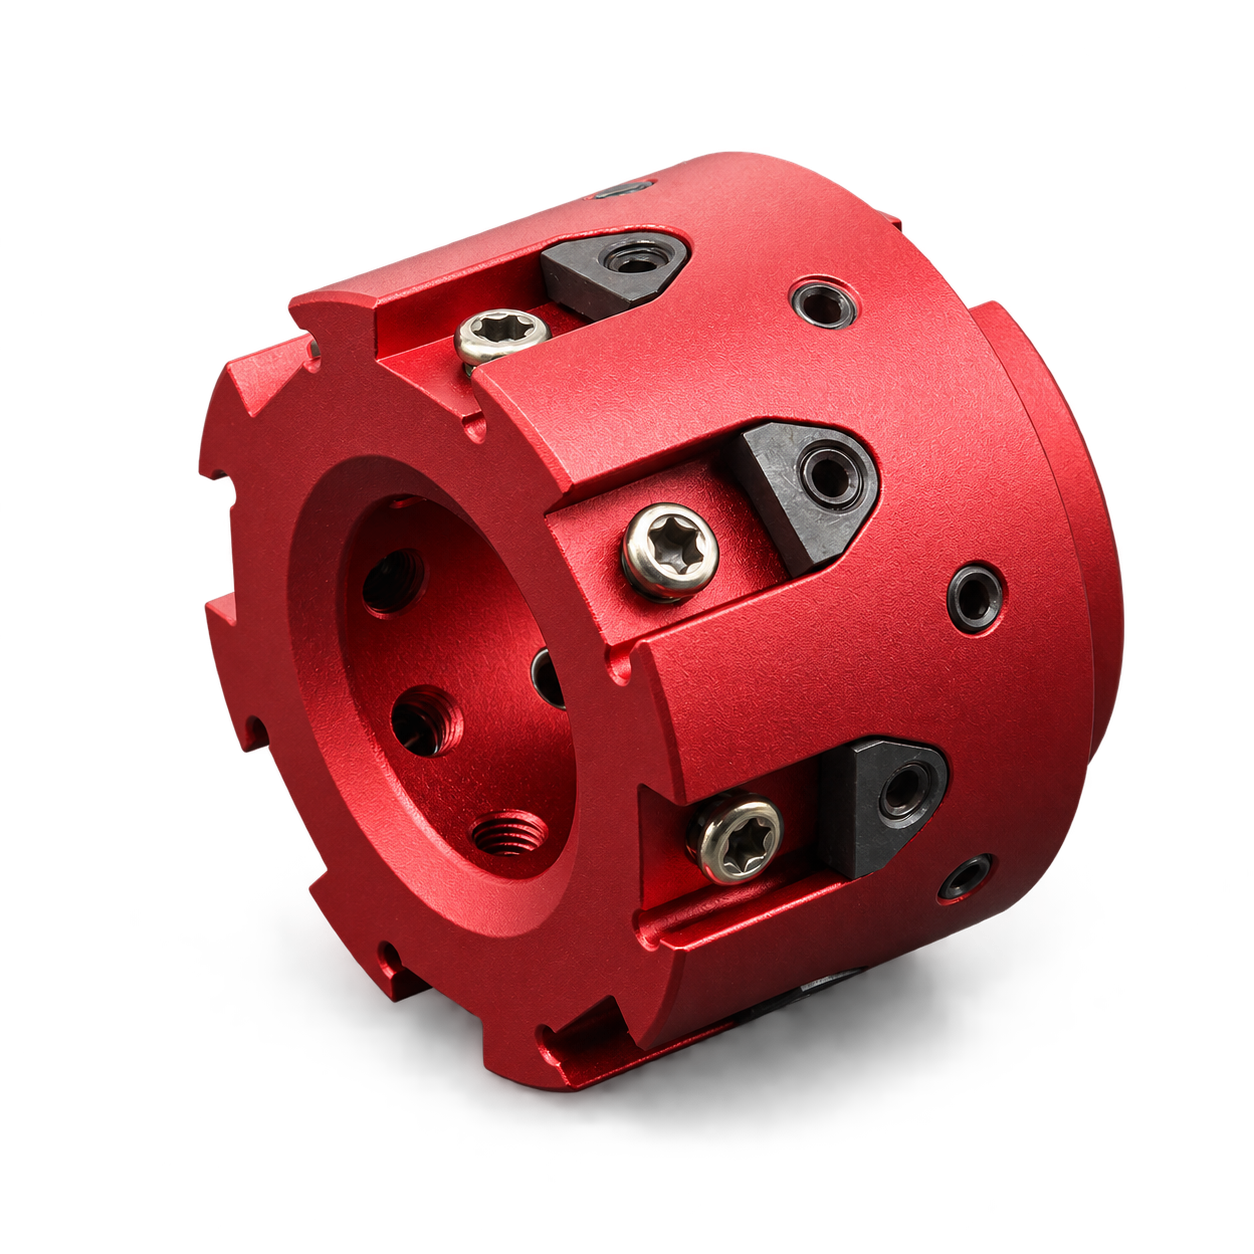
MSF-D — Fine-Pitch Adjustable PCD Face Milling Head
Fine-pitch adjustable heads with closer tooth spacing and wiper options. Available in Ø63–250 mm. MSF-D has more cutting teeth at the same diameter than the coarse-pitch MSF-S series.
View Details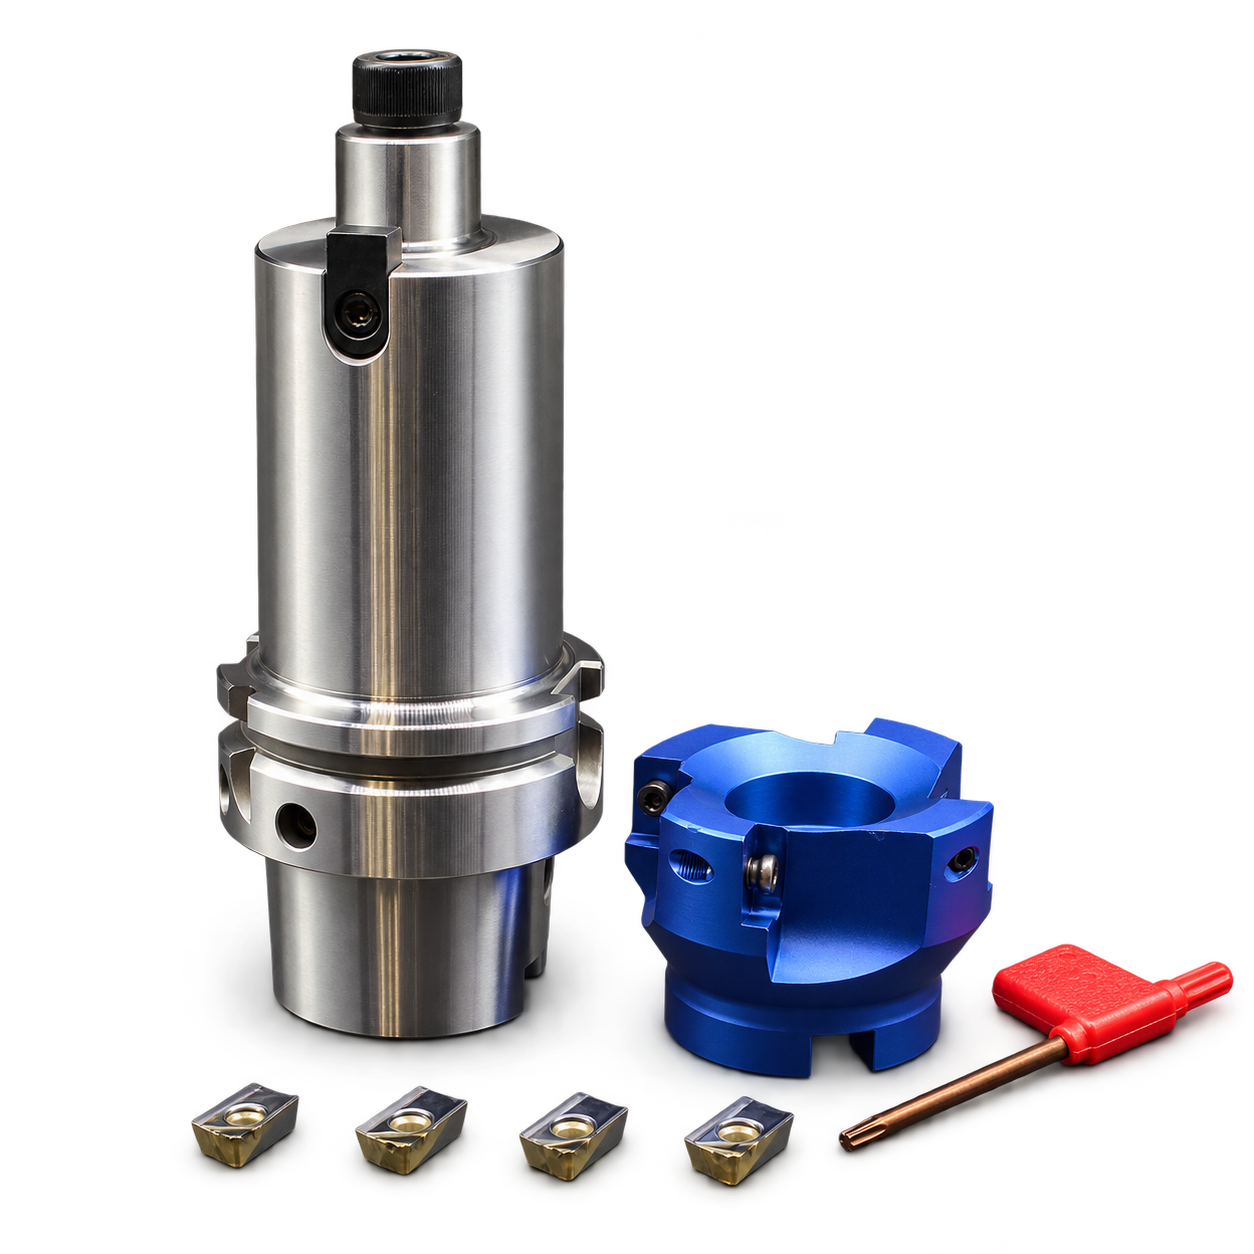
MFX — Fixed Face Milling Cutter
Fixed face milling cutter with matching APKT PCD inserts. Catalogue range Ø40–250 mm. Choose when a fixed pocket layout and APKT consumables fit the machine and cost model.
View DetailsCUTTING INSERTS & CARTRIDGES
PCD Cutting Inserts & Cartridges
MSW-PCD is a replaceable cartridge (cartridge body with PCD cutting edge), not a loose insert. MSF-PCD and APKT remain cutting inserts for their matching cutter bodies. Order inserts or cartridges with the cutter body; match designation, mounting and wiper duty before release to production.
MSW-PCD Cartridges
Wiper-oriented PCD cartridges for face-finish passes. Pair with the adjustable head and finish target on the order. Share your cutter model and current cartridge designation so we can confirm the match.
View Details
MSF-PCD Cutting Inserts
Primary cutting PCD inserts for the MSF adjustable platforms. Share current insert designation to confirm the match.
View Details
APKT PCD Cutting Inserts
APKT-style PCD inserts for MFX fixed cutters. Confirm body pocket and APKT designation together.
View Details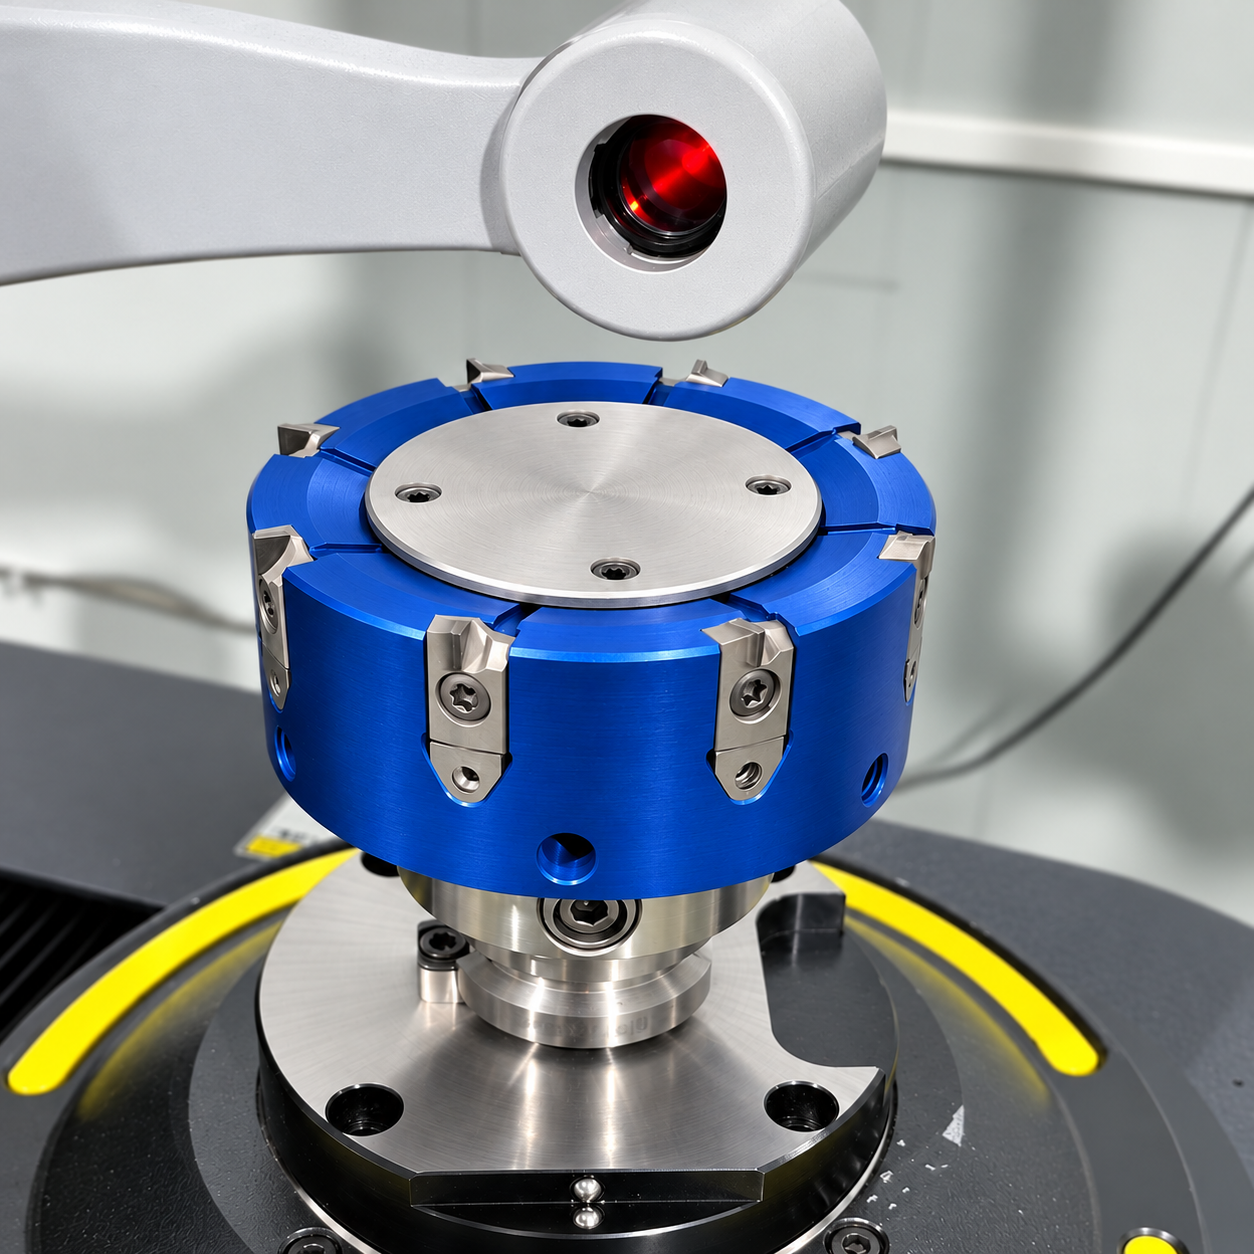
01 / BEFORE DELIVERY
Inspection & Cutting-Tip Presetting
Before delivery we confirm the agreed cutter configuration and preset cutting-tip heights. Total tip-height difference is held to ≤ 0.01 mm so installation starts from a measured set, not open tip-setting on your spindle.
Tip Height Difference
≤ 0.01 mmTotal difference between cutting tips after presetting. Tool-setting measure only — not a workpiece flatness tolerance.
Wiper Configuration
Confirmed against your Ra/flatness target for the selected head.
Interface & Cartridges
Mounting interface, cartridge and installation dimensions per standard or adapted design.
On-Machine Check
Verify the installed tool on your machine before production.
02 / IN APPLICATION
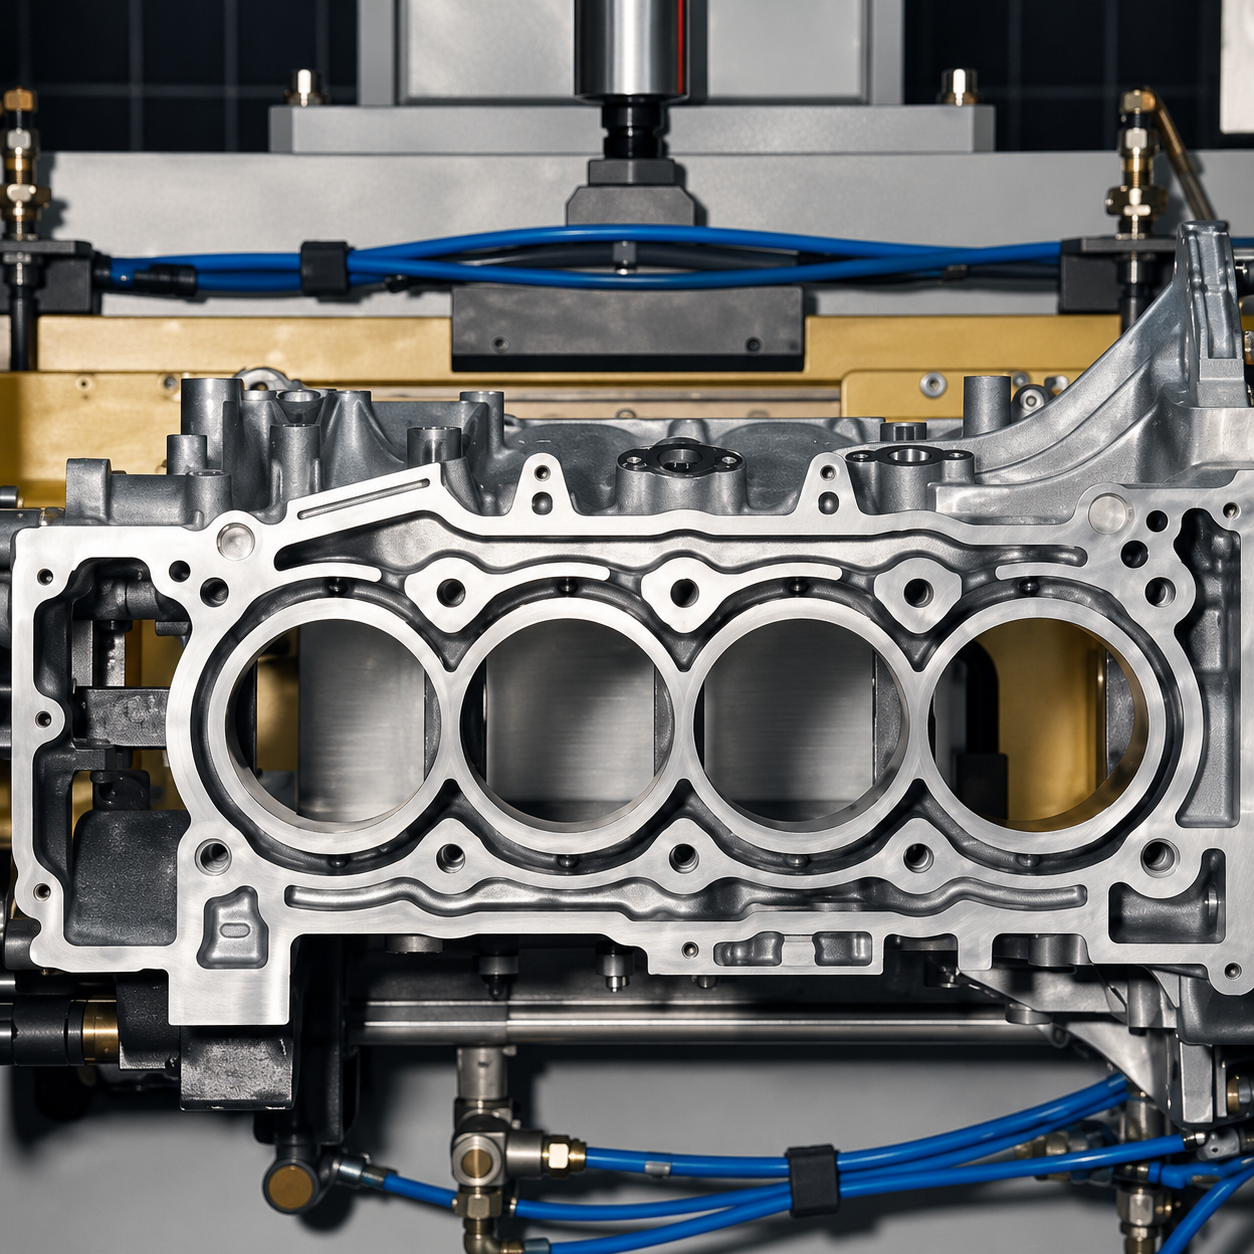
Face Milling for Cast Aluminum Cylinder Blocks & Heads
Cast-aluminum cylinder-block and head faces — interrupted cuts, finish targets and spindle limits — drive cutter series, wiper layout and starting Vc/fz/ap from Table A below.
Besides cast aluminum, SUNDI supplies indexable PCD face mills for copper, CFRP, other non-ferrous alloys, wood and selected ceramic-board jobs. Cutting data for those materials is quoted from the grade and drawing; aluminum Vc tables are not copied across. See Table B.
Cast Aluminum Components
Share casting grade, face to be milled and interrupted features.
Surface Requirements
State Ra and flatness separately; we match wiper and conditions to those targets.
Machine & Fixture Fit
Spindle interface, clearance and fixture limits before choosing or adapting the body.
Cutting Conditions
Set Vc, fz, ap and coolant together using Table A (cast aluminum) or quoted data for Table B materials.
CUTTING DATA
Starting Parameters by Material
For cast-aluminum face milling, SUNDI starting Vc is typically 800–3000 m/min at low silicon (about 4–9% Si) with PCD010, and 300–800 m/min at high silicon (about 14–18% Si) with PCD025 preferred. Always convert rpm from Vc and cutter diameter.
Table A is the published starting table for cast aluminum. Table B lists other materials we face-mill — RFQ fields only, not aluminum numbers.
Table a — Cast Aluminum Starting Values
| Silicon content | Suggested PCD grade | Vc (m/min) | fz (mm/tooth) | ap — finish (mm) | ap — roughing guidance (mm) |
|---|---|---|---|---|---|
| Approx. 4–9% Si | PCD010 | 800–3000 (typical 1500–2500) | 0.05–0.20 | 0.2–1.5 | 2–3 or more if spindle rigidity and load capacity permit; below 2 with limited rigidity. |
| Approx. 9–14% Si | PCD010 / PCD025 | 800–2500 | 0.05–0.20 | 0.2–1.5 | 2–3 or more if spindle rigidity and load capacity permit; below 2 with limited rigidity. |
| Approx. 14–18% Si | PCD025 (prefer over PCD010) | 300–800 | 0.05–0.20 | 0.2–1.0 | 2–3 or more if spindle rigidity and load capacity permit; below 2 with limited rigidity. |
- Starting recommendations for indexable PCD face milling on cast aluminum. Finishing ap and roughing ap serve different purposes.
- Actual ap depends primarily on the machine spindle’s rigidity and load capacity. With sufficient rigidity, 2–3 mm or more may be feasible; with limited rigidity, keep ap below 2 mm. Confirm the depth on the customer’s machine and setup.
- Catalogue maximum ap values (MSF-S ≈ 7 mm / MSF-D ≈ 5 mm) describe theoretical tool limits, not recommended operating depths or a guarantee that the machine can sustain the cut. Stay within the limit specified for the selected cutter body.
- Use wet cutting / through-coolant when the cutter and machine support it.
- Derive spindle speed from Vc and diameter; confirm that body’s n max before production.
- For high-silicon cast aluminum, reduce Vc if wear rises.
Table B — Other Materials: Scope & Rfq
| Material | Typical face-milling jobs | What to send in the RFQ | Cutting data |
|---|---|---|---|
| Copper & copper alloys | Housing faces, conductive parts, non-ferrous covers | Alloy, drawing, interface, finish target | Quoted for the grade and setup — not aluminum Vc |
| CFRP / carbon-fiber composites | Edge and face clean-up where PCD face mills apply | Layup/grade, drawing, delamination limits | Application-specific |
| Other non-ferrous alloys | Soft non-ferrous faces outside the Si bands above | Alloy designation, hardness/Si if known, drawing | Quoted per alloy |
| Wood & wood-based panels | Panel and pattern face milling where PCD heads are used | Material type, thickness, finish, machine limits | On request / selected jobs |
| Ceramic board | Special face milling | Board type, drawing, spindle limits, finish | On request / selected jobs |
Running copper, CFRP, wood or ceramic-board faces? Send the drawing and current tool list — we confirm series, inserts/cartridges and starting data for that job.
OEM Supply or Replacement Parts — Tell Us How You Buy
Distributors: established series plus application-specific modifications. End users: compatible inserts/cartridges so you can keep the body you already have. Uploads stay confidential.
SUPPLY & ENGINEERING SUPPORT
How We Work with Distributors & End Users
Two clear paths: OEM and adapted tooling for distributors, or compatible replacement components for a running production setup.
OEM & Adapted Tooling
Build your line on established cutter series, OEM supply and application-specific modifications. We configure from interface, dimensions and the job your customers run.
OEM Cooperation · Application-Specific Modifications
Replacement Parts
Compatible replacement inserts and cartridges for common tooling systems. After we confirm the current model, dimensions and photos, you keep the cutter body or toolholder and avoid replacing the full assembly.
Retain Compatible Cutter Bodies & Toolholders
Tell Us How You Work
application, current tooling, mounting dimensions, OEM or replacement need.
Review Options
established designs, required modifications, compatibility.
Confirm the Supply Plan
configuration, inspection needs, quantity and delivery schedule.
Frequently Asked Questions
Can a Standard Cutter Be Adapted to My Setup?
Yes. We modify established designs to your mounting interface, dimensions and application. Send the part drawing and installation constraints; we confirm what can change on the current platform versus what needs a new design.
Are the Cutting Tips Adjusted Before Delivery?
Yes. Tip heights are preset before delivery with total tip-height difference ≤ 0.01 mm. Confirm cutting-edge and wiper arrangement on the order, then verify the installed tool on your machine before production.
Can You Replace My Existing Inserts or Cartridges?
Yes, for confirmed-compatible inserts and cartridges. Send the current part number, mounting dimensions and photos before running them on an existing body. MSW-PCD is supplied as a cartridge, not a loose insert.
Which Specifications Are Available From Stock?
Some standard specifications are stocked; many configurations are made to order. We confirm availability and lead time against the selected model, modifications and quantity.
Do You Only Face-Mill Cast Aluminum?
No. Cast aluminum is our most documented application on this page. We also supply indexable PCD face mills for copper, CFRP, other non-ferrous alloys, wood and selected ceramic-board jobs — cutting data for those materials is quoted from your grade and drawing (Table B).
Do You Supply Distributors and End Users?
Yes. Distributors get OEM supply and adapted configurations on established designs. End users get application-specific cutter selection or a compatibility check for replacement components.