










Selection and influence of the number of end mill flutes
End mills are a type of cutting tool used extensively in the machining industry to shape and cut materials. These tools come in various configurations and sizes, each designed for specific purposes.The number of flutes on an end mill can significantly influence its performance, including cutting speed, finish quality, and tool longevity. Choosing the appropriate flute count is crucial for optimizing machining efficiency and achieving the desired outcome.In this article, we’ll take a closer look at “2-flute vs. 4-flute” end mills (as well as all other flute counts), exploring their unique advantages, limitations, and special features.

Basics of End Mill Flutes and Factors Influencing Flute Selection
Flute count is critical to end mill performance, affecting core size, durability, chip evacuation and surface finish. Understanding the basics of flute count is critical to selecting the right tool, whether you are machining aluminum or steel, roughing or finishing.
Flute count describes the number of cutting edges around an end mill. In a solid end mill, these edges are not separate inserts.
For comparable diameters, flute count and core design create a trade-off between cutting-edge capacity and chip space.
More flutes do not inherently improve chip evacuation.
Select the geometry and coating for the material and cut, not from flute count alone.
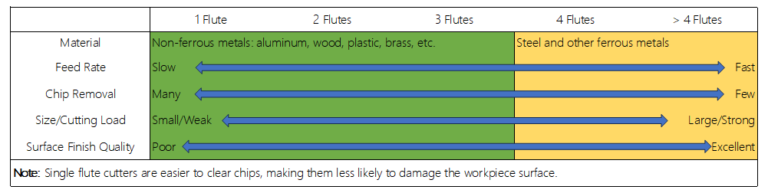
The effect of the number of cutting flutes and the depth of chipformer flutes in end mills
Flute depth and core geometry affect both chip space and tool rigidity. Heavy-engagement cuts need sufficient evacuation space. Light-engagement cuts may accommodate more flutes. Roughing or finishing alone does not determine the correct count.
Relationship between flute number and material removal rate of end mills
Flute count alone does not determine removal rate or finish. At a fixed spindle speed and feed per tooth, more teeth increase the programmed feed rate, but only if the tool and process can sustain that load. Engagement, rigidity, runout, and chip clearance must also be considered.
2 flute end mill vs 4 flute end mill
2-flute and 4-flute end mills are commonly used for machine tool machining, and each has unique advantages and limitations depending on the material and operation. In the following sections, we’ll explore these differences in more detail to help you make an informed decision when choosing between 2-flute and 4-flute end mills for your specific needs.
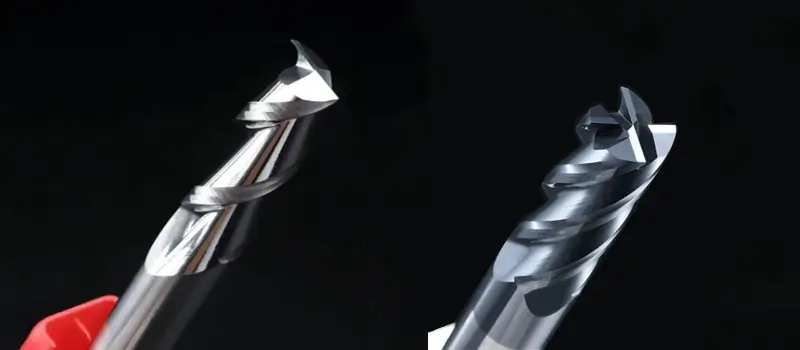
What is a 2 flute end mill used for
Two-flute end mills are often selected for slots and pockets in aluminum when chip clearance is important. Choose an appropriate material-specific geometry and coating.
Two flutes do not automatically produce larger chips, higher cutting speeds, or longer life; these results depend on the cutting conditions and tool design.
What are 4 flute end mills used for
Four-flute end mills are common options for steel machining. Confirm the specific tool’s suitability for slotting, side milling, or finishing.
Flute count does not establish heat resistance; select the grade, coating, and cutting data for the work material and operation.
single flute end mill and triple-flute end mill
Single-flute and three-flute tools are available for aluminum and other materials.
A single flute can provide substantial chip space.
At the same RPM and feed per tooth, three teeth permit a higher programmed feed than two, subject to chip clearance, power, and rigidity limits.
End mills with more than 4 flutes
Tools with more than four flutes can suit low-engagement strategies and selected finishing operations. Material-specific designs are available for steels, titanium, and nickel alloys. Use the maker’s guidance; these materials cannot be grouped by hardness alone, and a higher flute count is not automatically suitable for a deep slot.
Factors to consider when selecting the number of flutes: When selecting the appropriate number of flutes, consider factors such as the type of material, machining operation and tool life to ensure optimum performance.
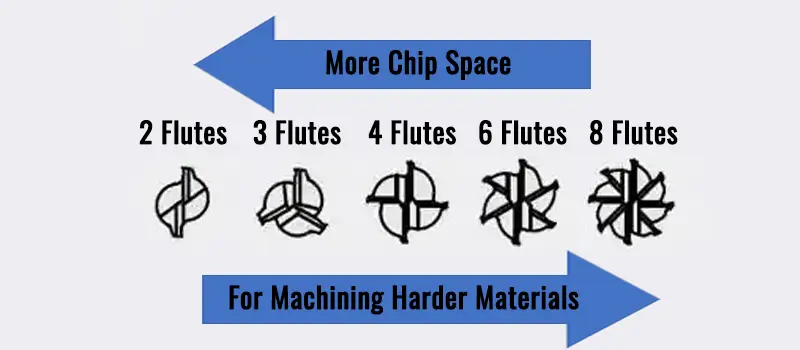
Factors Influencing Flute Selection
When selecting the appropriate number of cutting edges, consider factors such as material type, machining operations and tool life to ensure optimum performance.
Type of material
Consider the specific alloy or non-metallic material, its chip behavior, and the cutting operation. Hardness alone is insufficient.
Start with material-specific tooling recommendations, then check chip space and allowable engagement for the intended process.
Machining process
Distinguish full-slot cutting, side milling, and low-engagement roughing when selecting flute count.
A dedicated multi-flute HEM tool can rough effectively in its intended application. Finishing may benefit from additional teeth, but surface quality and cutting force are not guaranteed by tooth count.
Tip: Use end mills with more chip evacuation flutes in aluminum
Aluminum side milling may use higher flute counts when tool design and engagement provide adequate chip clearance. There is no universal four-flute limit: specialized five-flute aluminum tools are available for HEM. Side milling can still suffer chip packing, so validate engagement, chip evacuation, and cutting data.
End mill flute count affects tool life and performance
Do not assume that adding flutes extends tool life. Compare suitable cutters under defined conditions and measure wear, part quality, and productive cutting time.
Choose the count as part of the complete tool-and-process selection.