










A Complete Guide to Milling Cutter Tools
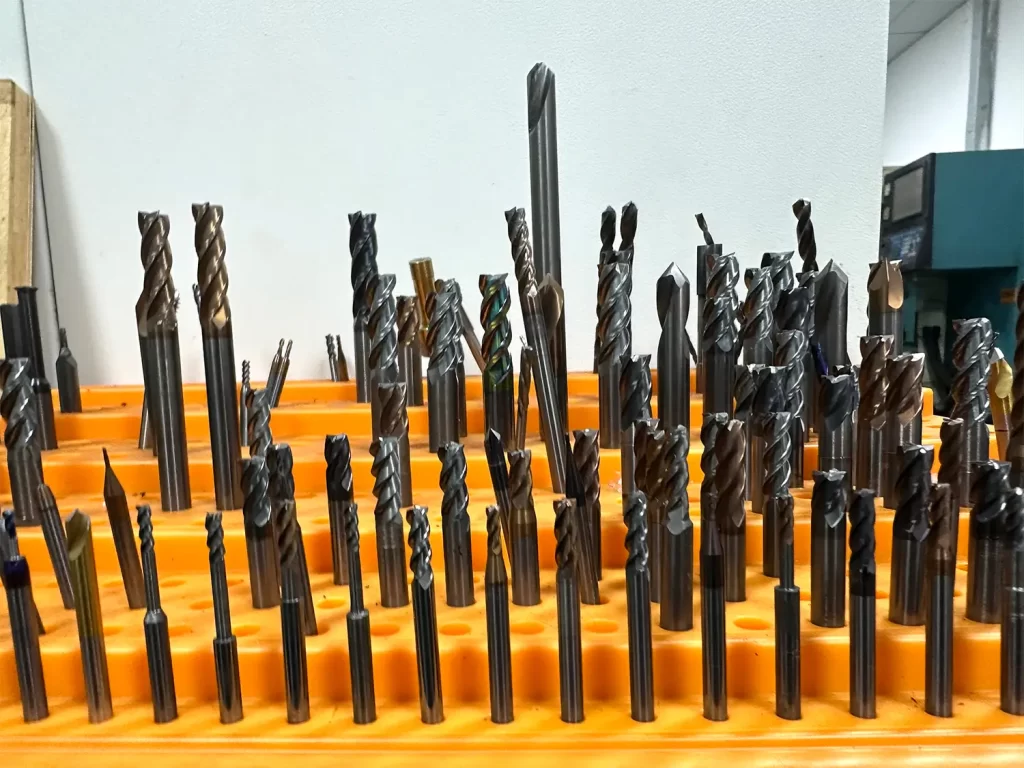
In machining, end mills are super popular because they’re so versatile and useful, making them the most commonly used cutting tool. For a lot of machining newbies, they’re often the first tool to try. There are so many different kinds of end mills, so in this article, we’re diving into the basics and some tips to help you pick the best one. This will help you choose the most cost-effective and efficient end mill for your needs, whether you’re buying or using them!
Contents
What Are Milling Cutter Tools?
Milling cutters remove material by rotating cutting edges. End mills are one family, used for features such as slots, pockets, and profiles. Solid HSS or carbide tools and tipped or indexable constructions serve different applications. PCD and CBN are cutting materials, not interchangeable upgrades: select the grade and geometry for the workpiece, operation, and machine.

Types of Milling Cutter Tools
Milling cutters come in various types, each designed for different applications and performance levels. Choosing the right milling cutter based on your specific needs is crucial. Below are some common types of milling cutters. You can quickly refer to the table for an overview.
| Category | Type | application | |
|---|---|---|---|
| END Mill | Square end mills |  | They’re perfect for operations like slotting, edge milling, and contouring, especially when it comes to making right-angle edges and flat-bottomed grooves. |
| Ball nose end mill |  | They’re ideal for high-precision finishing of smooth curved surfaces, 3D profiles, and complex contours. | |
| Bull nose end mills |  | Used to form an internal corner radius; distinct from an external corner-rounding cutter. | |
| Rounding end mills | 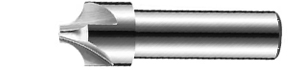 | Used to form external edge radii. A straight chamfer requires a different geometry. | |
| Undercutting End Mills | 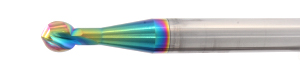 | Used for machining undercuts, grooves, overhangs, or complex parts with hard-to-reach geometries. | |
| Micro end mills |  | Ideal for micro-machining, electronic components, medical devices, and micro-mold manufacturing. | |
| Face Mills | Face Milling cutter | 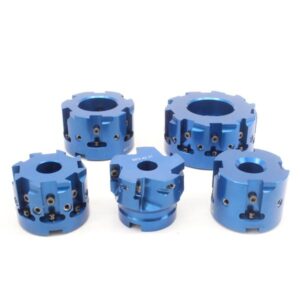 | Perfect for large-area flat milling, capable of both efficient rough machining and high-precision surface finishing. |
| Slotting Cutters | T-Slot Cutters | 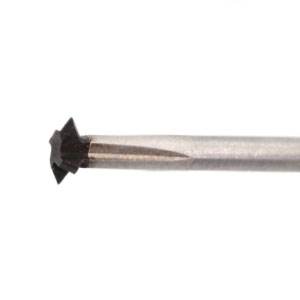 | Ideal for machining T-slots, used for fixture fixing or the installation and positioning of sliding mechanisms. |
| Saw Cutters | 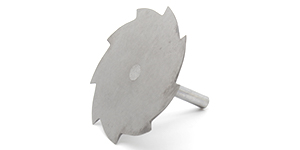 | Ideal for high-precision machining of deep, narrow slots or separating thin workpieces. | |
| Specialized Cutters | Dovetail cutter | 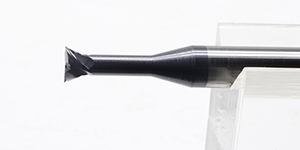 | Used for dovetail slots with a trapezoidal cross-section. |
| Thread milling cutters | 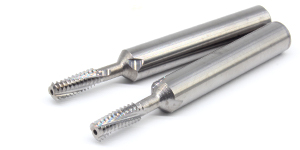 | Ideal for internal and external thread machining. | |
| Concave and Convex Milling Cutters | 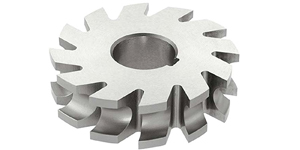 | Ideal for machining concave or convex curved profiles on workpieces, commonly used in mold and decorative processing. | |
| Cylindrical Milling Cutter | 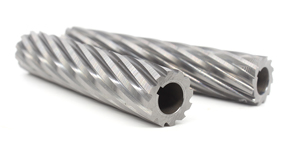 | Mainly used for large-area flat milling or precision profile machining. |
Next, let’s take a closer look at each type of milling cutter in detail.
1. End Mills
End mills commonly cut with peripheral and end edges. Permitted feed directions depend on the design; axial plunging requires a tool rated for that operation, and not every end mill is centre-cutting.
1.1 Square end mills
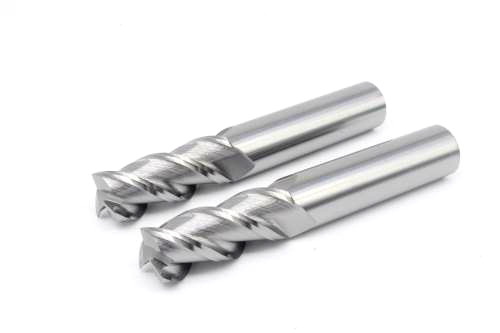
Also known as flat end mills, square end mills have a flat tip and a 90° cutting edge angle. If you’re dealing with tasks like slotting, pocketing, or profiling, these tools are a great choice.
1.2 Ball nose end mill
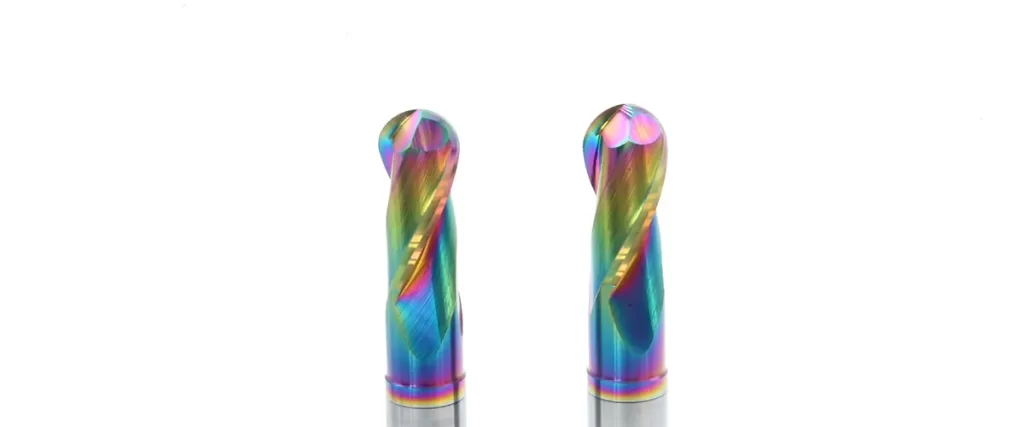
Also called a ball end mill, it has a hemispherical tip, and its rounded cutting edges are perfect for smooth surfaces or 3D contouring. It is especially suitable for machining the contours of injection molds used in silicone seals.
1.3 Bull nose end mills
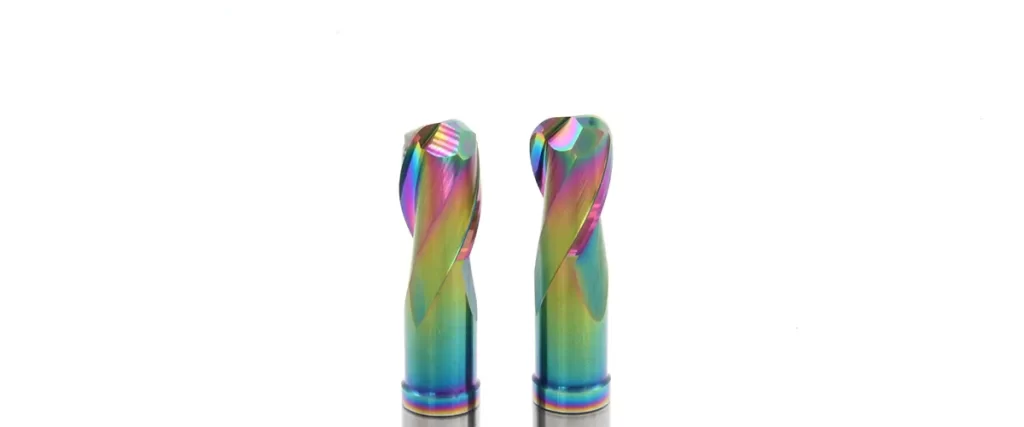
Also known as corner radius end mills, these tools have a radius joining the end and peripheral cutting edges. This can strengthen the corner and form an internal corner radius; it is distinct from rounding an external part edge with a corner-rounding cutter.
1.4 Rounding end mills
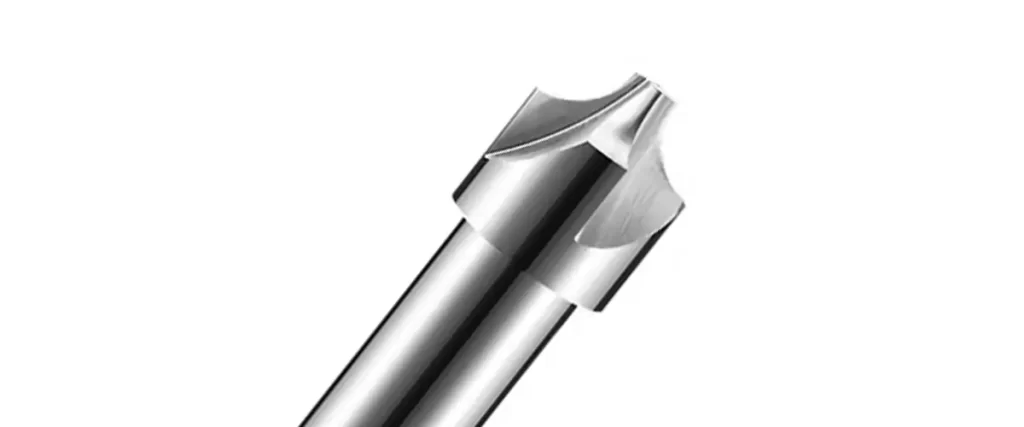
Corner-rounding end mills produce an external edge radius using a matching form. A radius and a straight chamfer are different features; select the cutter for the drawing.
1.5 Undercutting End Mills
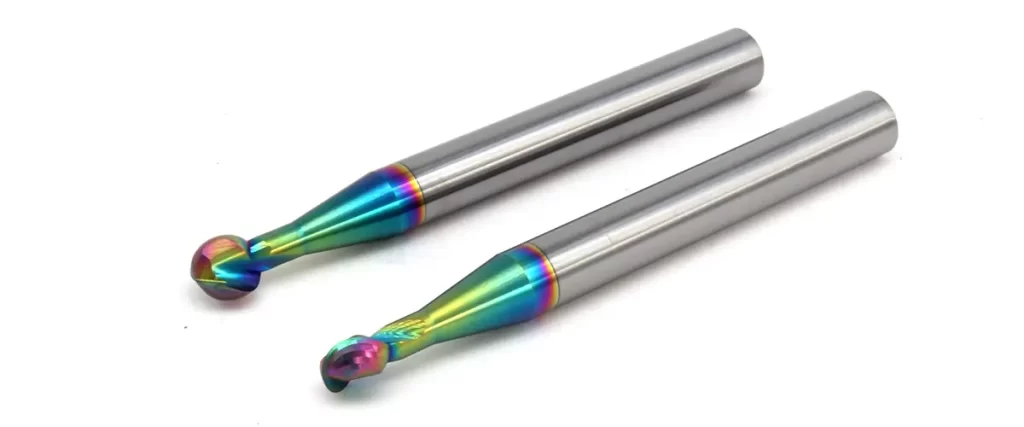
The tip is spherical, kind of like a lollipop, which is why they’re also called lollipop cutters. They’re mainly used for machining hard-to-reach areas and parts with undercut structures, like in the mold-making industry.
1.6 Micro end mills
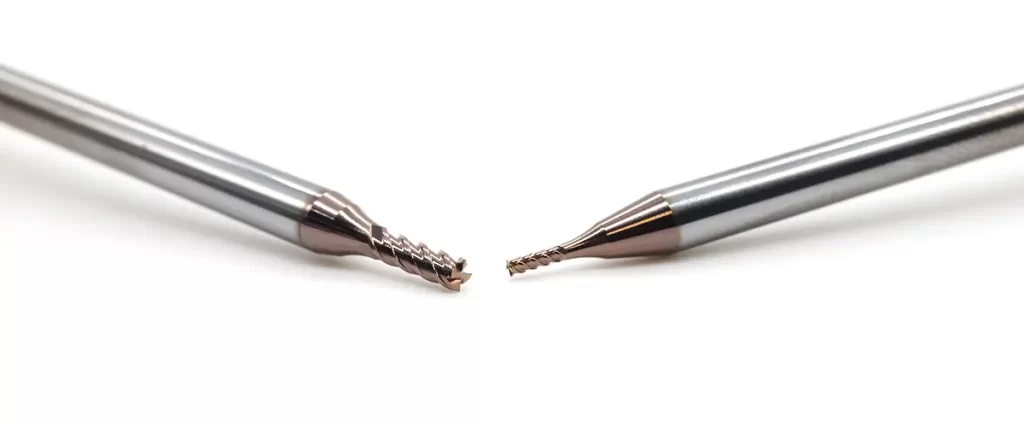
Micro end mills machine small features in applications such as electronics, medical components, and micro-moulds. The size boundary varies by catalogue; 4 mm is not a universal definition. Dental component manufacture also uses specialised milling tools, which should not be confused with instruments used directly on teeth.
2. Face Mills
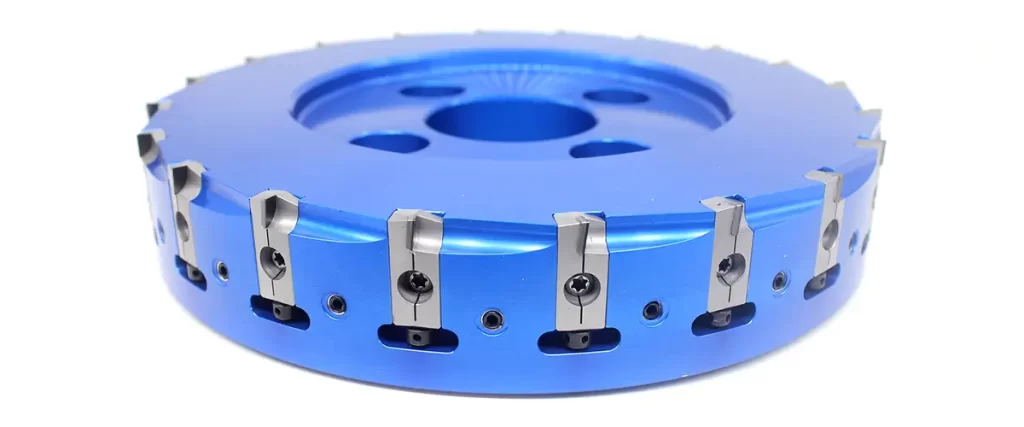
Face mills machine flat faces and are available in many constructions and cutting materials. Adjustable and brazed PCD Face Milling tools are examples, not the only two types. Brazed tips are not necessarily interchangeable inserts; select the cutter for material compatibility, removal rate, and finish.
3. Slotting Cutters
Slotting cutters are milling tools designed for cutting slots or narrow grooves.
3.1 T-Slot Cutters
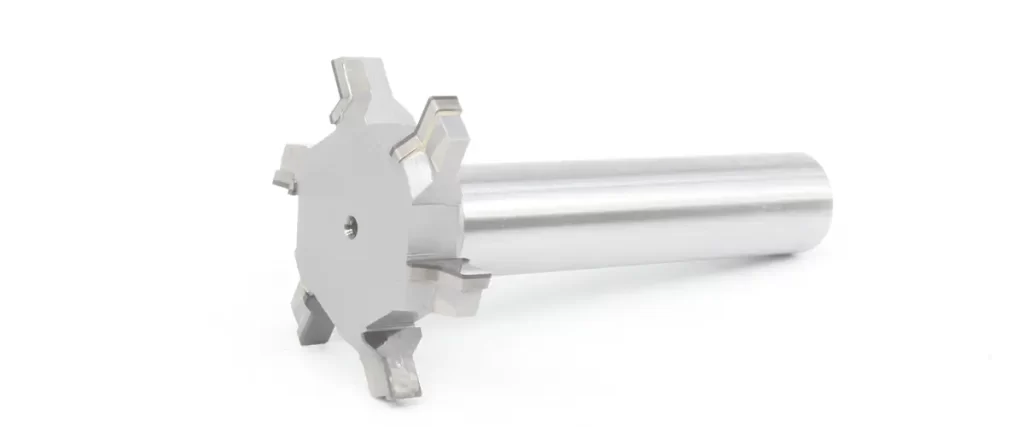
T-slot cutters have a disc-like cutting head wider than the neck. They machine the wider undercut portion of a T-slot; access and the preceding straight slot must suit the tool and feature.
3.2 Saw Cutters
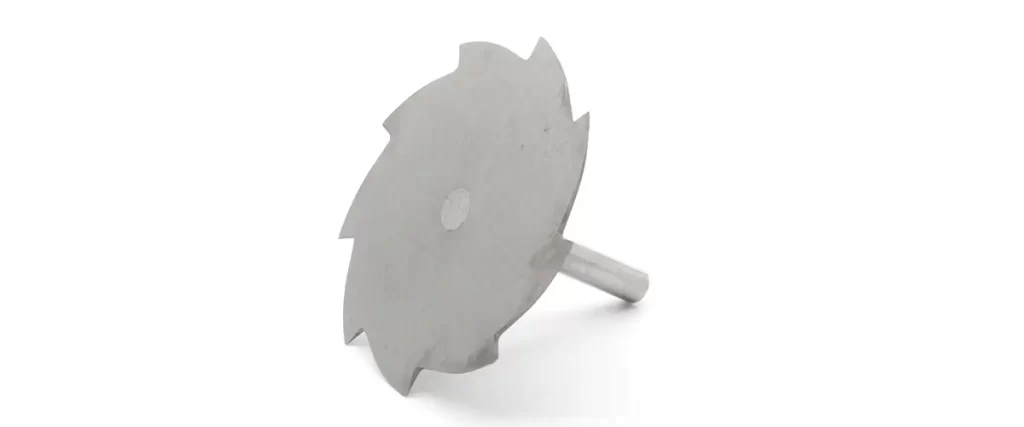
The blades are thinner, designed for machining narrow grooves or slots with a depth greater than the blade thickness.
4. Specialized Cutters
Specialised milling cutters serve particular features and operations. Many are standard catalogue tools rather than custom or non-standard end mills.
4.1 Dovetail cutter
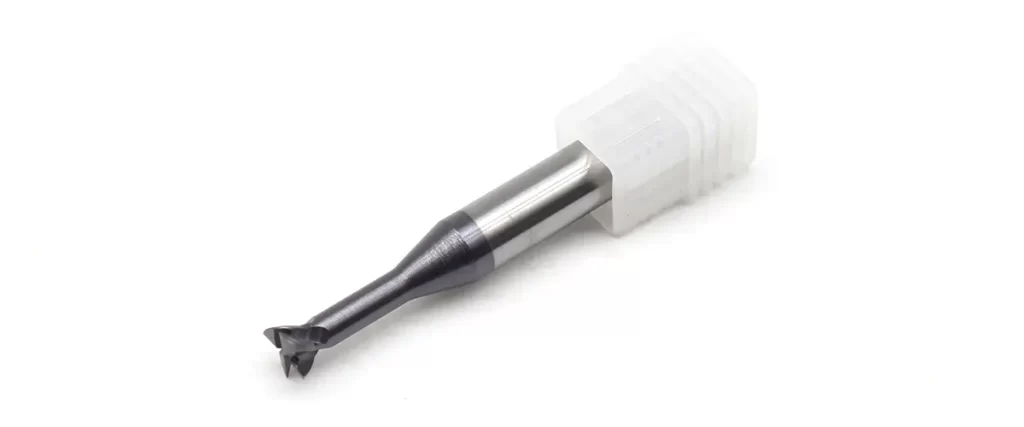
A type of forming end mill, it has a wide tip and a trapezoidal cutting edge, specifically designed for machining dovetail slots. It can cut dovetail structures with a trapezoidal cross-section, often used in the processing of sliding components or fixed connections.
4.2 Thread milling cutters
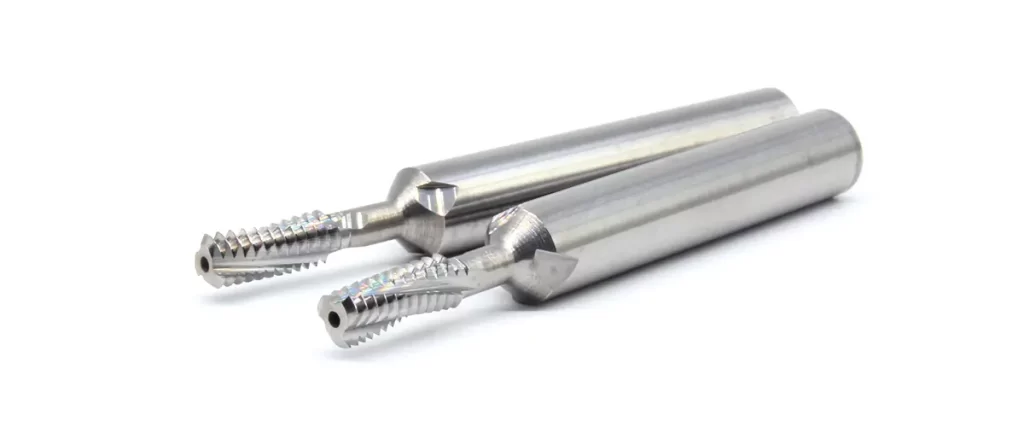
A thread mill machines threads using a compatible interpolated path. Internal and external capability depends on its design, diameter, thread form, and machine control; it is not universally more stable than tapping.
4.3 Concave and Convex Milling Cutters
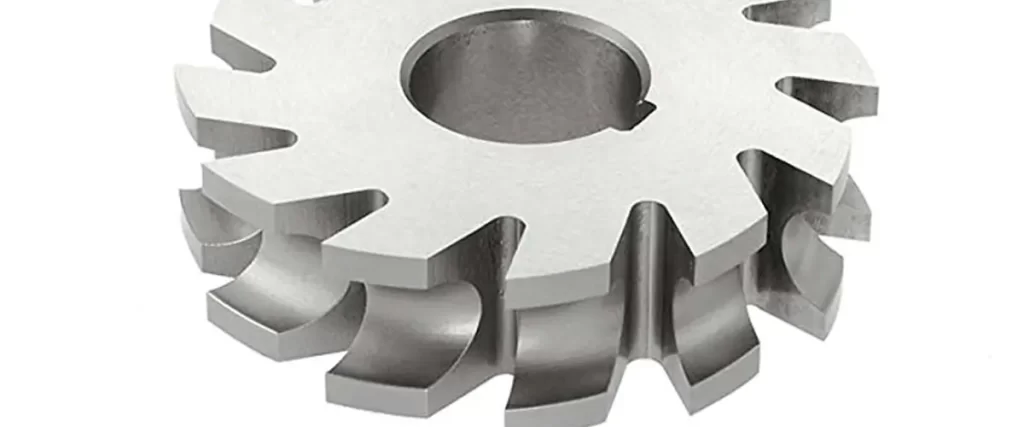
A type of forming end mill, it’s specifically designed for machining curved profiles on the surface of a workpiece.
4.4 Cylindrical Milling Cutter
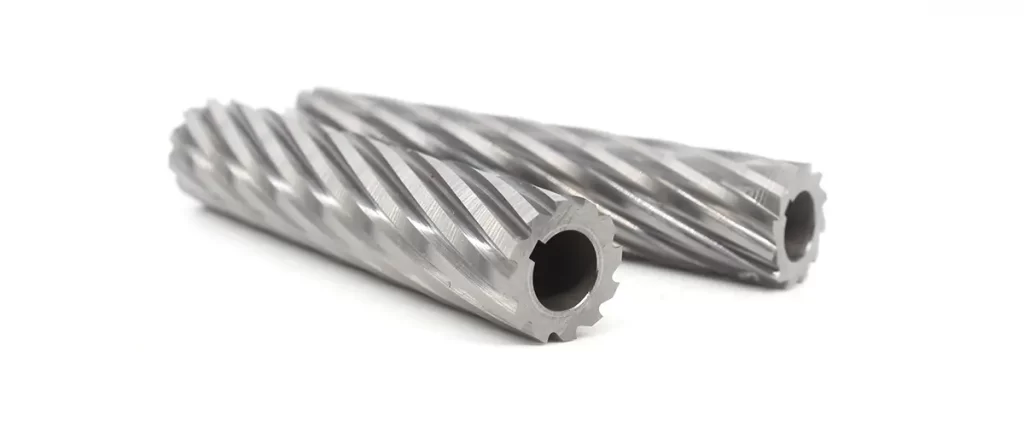
The cutting edges are distributed along the outer perimeter of a cylindrical body, making it ideal for milling flat surfaces or large areas of a workpiece.
Milling Cutter Material Options
Tool construction and cutting material are separate choices. Solid, brazed-tip, and mechanically retained insert designs can use different cutting materials. HSS, carbide, PCD, and CBN must be selected for the application; PCD and CBN do not define every insert-type cutter.
1. Solid Milling Cutters
1.1 HSS milling cutter
High-speed steel (HSS) comprises grades with different alloying and hot-hardness properties. It can be a tough, resharpenable choice at suitable cutting speeds. Neither a single 600°C limit nor lower accuracy than carbide is universal; select cooling and cutting data for the grade, operation, and workpiece.
1.2 Cemented Carbide Milling Cutter
Cemented carbide commonly combines tungsten carbide particles with a cobalt-rich binder. Grade selection balances wear resistance and toughness. It often permits higher cutting speeds than HSS, but a 1000°C capability, longer life, or higher accuracy is not guaranteed for every tool and operation. Cast irons and non-ferrous alloys also vary widely in hardness and machinability.
1.3 Coated Carbide Milling Cutter
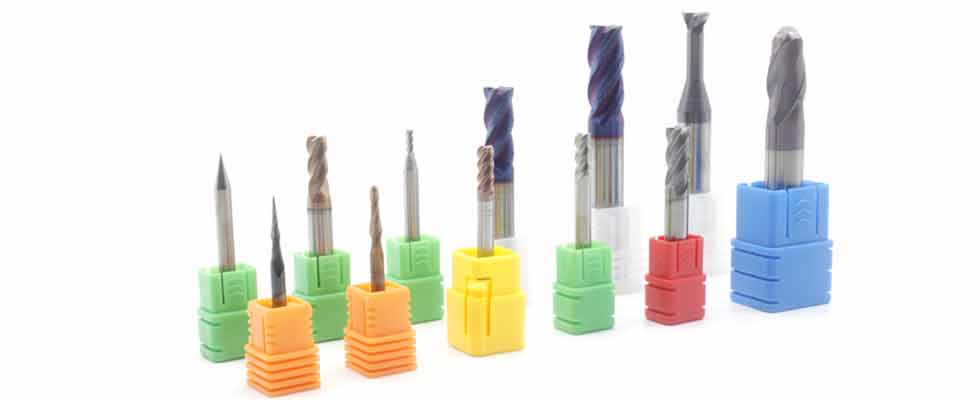
Carbide tools may carry coatings such as TiN, TiAlN, or AlTiN. Their suitability depends on the substrate, workpiece, temperature, and cutting conditions. Coating does not eliminate adhesion, oxidation, or wear, and the stated two-to-tenfold life increase needs application-specific test evidence.
2. Tipped Milling Cutters
2.1 PCD milling cutter
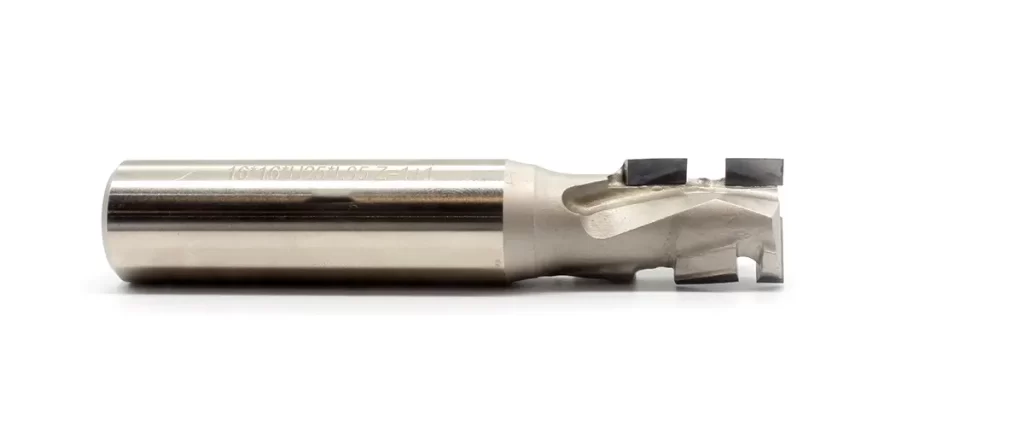
PCD consists of diamond grains bonded into a cutting material. It is useful in selected abrasive non-ferrous and nonmetallic applications, including suitable aluminium alloys, graphite, and composites. Do not interpret an unsupported 80–120 multiplier as a hardness ratio or assume chip blockage cannot occur. Thermal and chemical limits depend on the grade and process; interaction with iron is a major limitation in conventional steel cutting.
2.2 CBN milling cutter
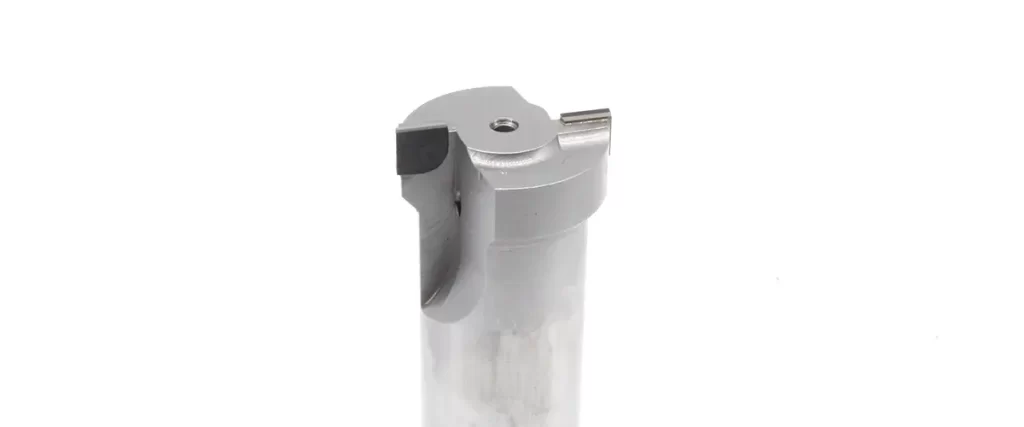
Cubic Boron Nitride (CBN) is a very hard cutting material used in suitable grades for applications such as hardened steels and certain cast irons. It is not the best choice for all steels, stainless steels, or titanium alloys. Edge sharpness is a matter of tool geometry and preparation, not an automatic consequence of hardness. Choose among CBN, carbide, PCD, and other materials for the actual application.
3.3 Carbide Tipped milling cutter
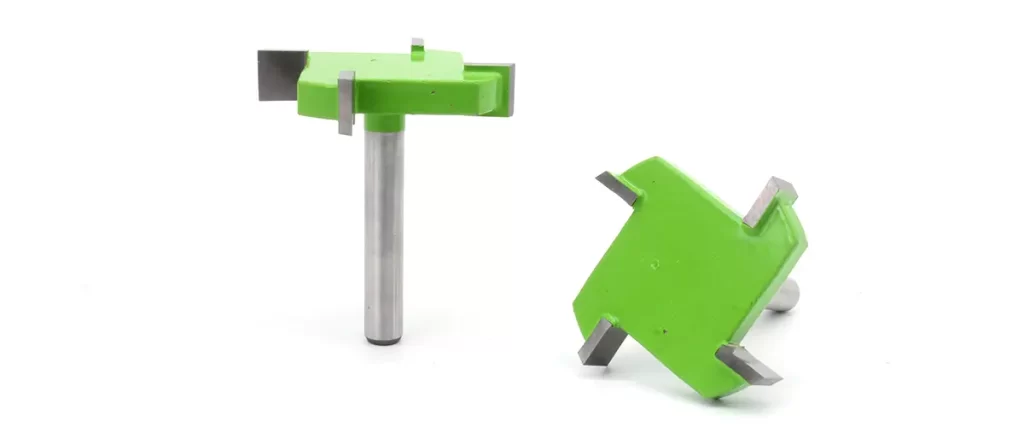
Carbide-tipped milling cutters combine carbide cutting portions with a supporting body, often steel. Construction and attachment vary. This can balance cost and cutting performance, but it is not invariably the lowest-cost milling solution.
Choosing the Right Milling Cutter
Above, we’ve introduced the different styles and material structures of milling cutters. If you’re still unsure about the characteristics of each type, feel free to quickly refer to the tool type chart above.
Of course, in actual machining applications, we must also take into account other factors, including processing conditions, machining requirements, and, importantly, economic efficiency.
1. Machining Conditions
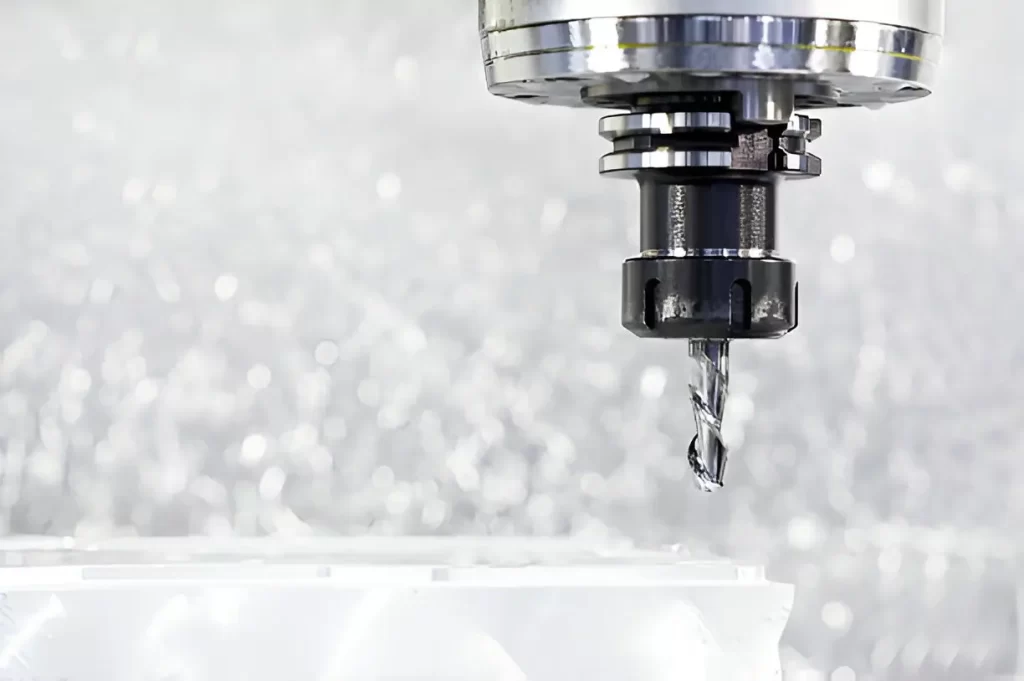
Check spindle speed, power and torque across the intended speed range, along with rigidity, toolholding, runout, and permitted tool dimensions. Determine RPM from cutting speed and diameter, then check machine and tool limits; cutter size alone does not establish power demand or a minimum usable speed.
2. Processing Requirements
2.1 Workpiece Material Requirements
Select cutting material and coating for the workpiece grade and operation. Carbide and PCD can suit different non-ferrous applications; PCD may also suit abrasive composites. Stainless steel and titanium are not generic reasons to choose CBN. Use the supplier’s application data rather than a soft-versus-hard material rule.
2.2 Surface Finish Requirements:
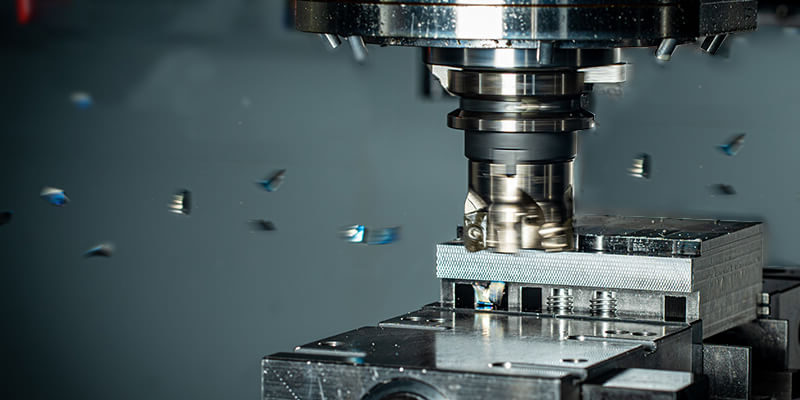
Roughing tools and engagement should support efficient stock removal within machine and setup limits. Finishing selection depends on the specified dimensions and texture; a larger rougher or a higher tooth count is not automatically better.
3. Tool Parameters
3.1 Milling Cutter Structure
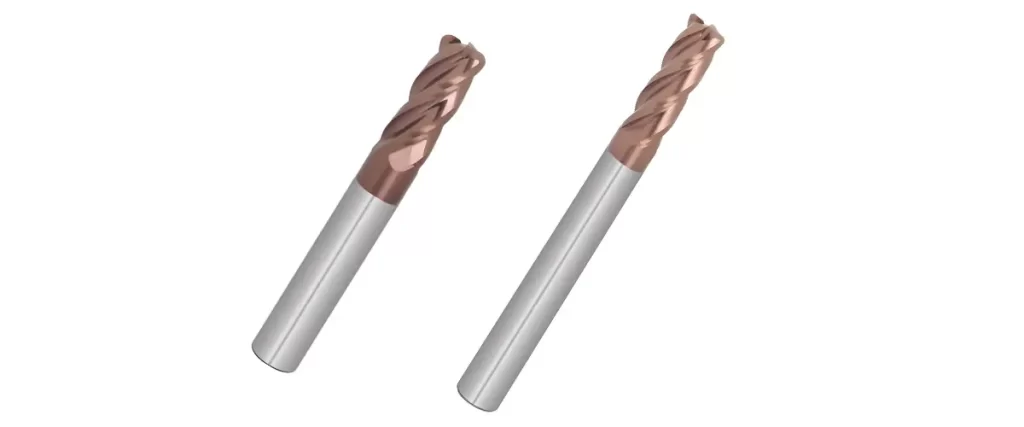
Solid and indexable cutters can both serve roughing or finishing when designed for the task. Use the shortest practical overhang: increasing unsupported length relative to diameter reduces stiffness. There is no general L/D boundary of one third. Distinguish axial depth of cut, ap, from radial engagement, ae; neither a fixed 0.3D limit nor automatically lowering speed and feed is a universal remedy for vibration.
3.2 Milling Cutter Coating
Select coatings by their specification and application, not colour alone. DLC (diamond-like carbon) may suit particular non-ferrous applications but is not interchangeable with diamond coating or PCD for abrasive composites. For further background, see “50 Tool Coatings for Different Materials.”
3.3 Number of Cutter Teeth
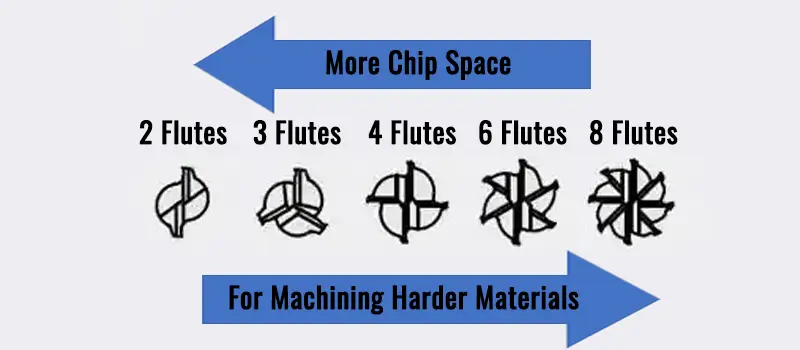
Flute count balances chip space, core strength, and productive feed. Both roughing and finishing tools are available with different counts; four or more teeth does not define a finishing tool. Match flute geometry and engagement to the material and chip volume.
3.4 Tool Geometry
The rake angle, cutting edge inclination angle, and relief angle should be matched according to the tool material, workpiece material, and machining conditions. A larger rake angle is suitable for softer materials like aluminum, while for harder materials like steel, a smaller rake angle helps improve cutting stability.
3.5 Economic Efficiency
Finally, choosing the right tool requires a careful balance of cost, lifespan, and tool change time. For smaller projects, using some cost-effective alternative brands can offer better cost efficiency. On the other hand, under specific production conditions, opting for tools with longer lifespans, like using PCD tools for aluminum machining, may be more expensive upfront. However, the longer tool life reduces downtime and replacement costs, ultimately providing better long-term cost efficiency, especially in high-volume or precision machining scenarios.
Conclusion
To wrap it up, milling cutters are one of the most widely used tools in machining, and their variety in types and materials makes them versatile across many industries. If you’re still unsure about which milling cutter is right for you, feel free to contact our SUNDI team. With decades of experience, our sales engineers can help you choose the perfect tool for your project and ensure you get top-quality results.
Got questions? Reach out now for a quote!