










Climb Milling Vs Conventional Milling
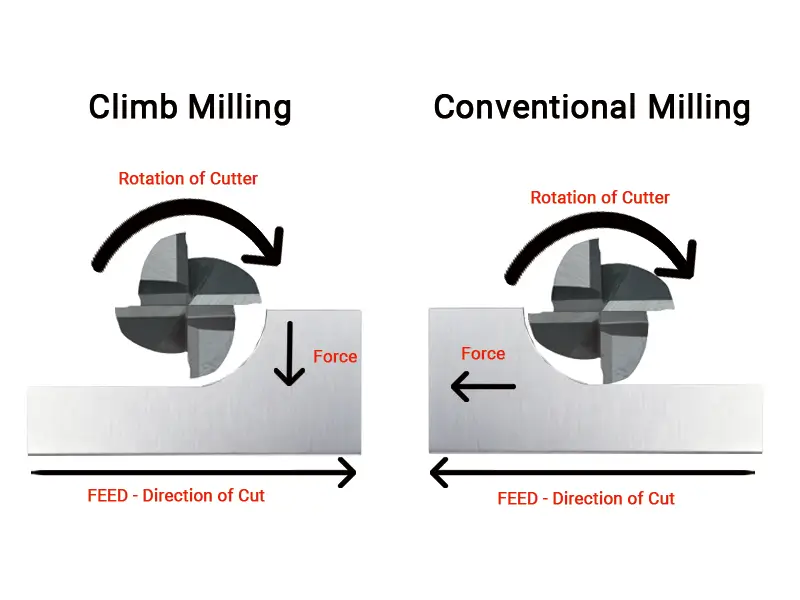
Climb and conventional milling describe the relationship between workpiece feed and the local cutting motion of the milling cutter. In peripheral climb milling these directions agree at engagement; in conventional milling they oppose one another. Force directions also depend on tool orientation and geometry.
Choose the method for the machine, workholding, material, and operation; neither has a universal cost advantage.
Contents
What Is Climb Milling
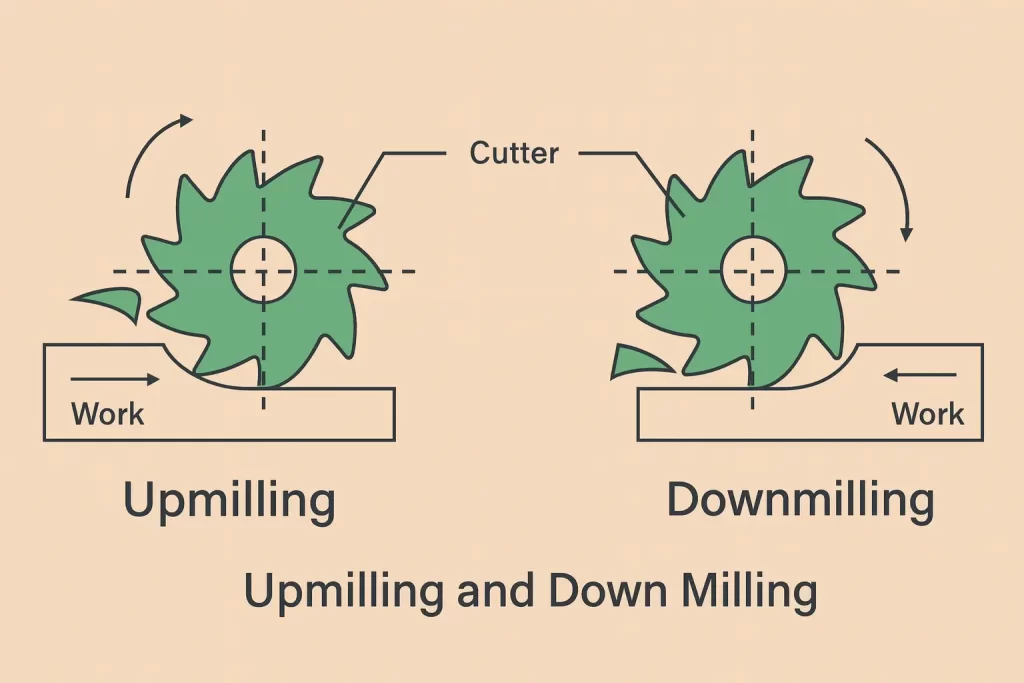
In peripheral climb milling, also called down milling, the cutting motion at engagement follows the workpiece feed direction. Chip thickness decreases from its initial value towards zero. Chip evacuation and exit conditions still depend on the toolpath and setup.
What Is Conventional Milling
In peripheral conventional milling, also called up milling, the cutting motion opposes the workpiece feed. Chip thickness starts near zero and increases, so rubbing can occur before a chip forms. Chip flow depends on the cutter and evacuation arrangements.
Advantages Of Climb Milling
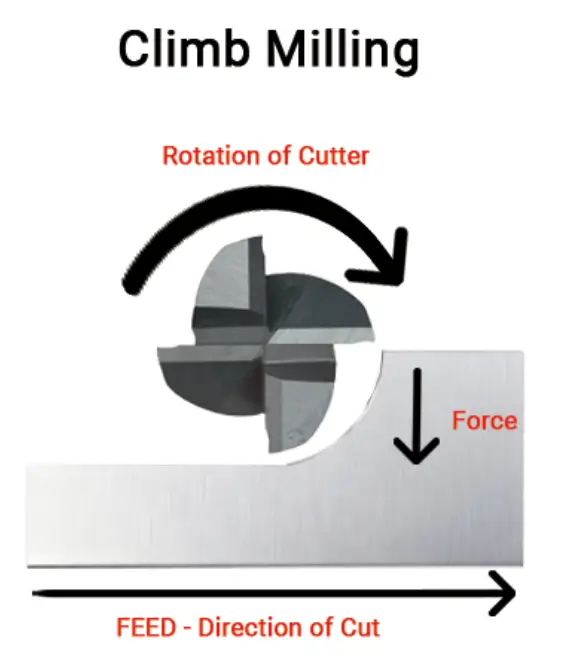
Climb milling is often preferred when the machine, fixture, and workpiece permit it. The following benefits depend on the actual operation.
Superior Surface Finish
Climb milling can improve finish by reducing entry rubbing. Chip recutting and deflection remain possible; compare measured surfaces rather than assuming a better finish in every case.
Extended Tool Life
Climb milling may improve tool life in a suitable process. The original 40–50% claim lacks defined test conditions and is not a general performance promise. Assess life using the same material, tool, cutting data, and wear criterion.
Reduced Cutting Forces
Climb milling can pull the workpiece into the cutter. Workholding must resist the actual force directions; do not reduce clamping solely because the cut is classified as climb milling. Spindle life and power savings are not guaranteed.
Better Chip Evacuation
Climb milling may reduce the likelihood of chip recutting in a suitable setup, but it does not eliminate it. Provide effective evacuation and check for chip packing and surface damage.
Lower Heat Generation
Chip thickness, rather than chip width, decreases through a conventional peripheral climb cut. Heat and dimensional effects depend on the complete process; choosing climb milling alone does not guarantee a cooler workpiece or tighter tolerances.
Disadvantages Of Climb Milling
Climb milling demands rigid machines and proper setup. If you get the setup wrong, bad things happen fast.
Backlash Issues
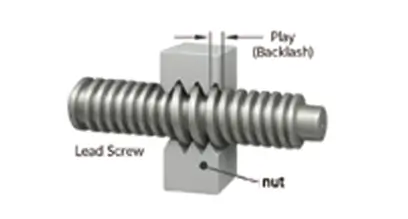
Climb milling can cause unintended feed movement when mechanical play allows the cutter to pull the workpiece into the cut. Check machine condition and permitted operating methods using the manufacturer’s procedure; machine age alone does not determine suitability.
Workpiece Stability Requirements
Climb milling pulls your workpiece toward the cutter. However, inadequate clamping leads to workpiece movement. Part shifts during the cut equal scrap parts. You need robust fixturing. Light workholding simply will not cut it.
Initial Tool Impact
The initial chip load must be appropriate for the edge and setup. Interruptions and rough stock require application-specific selection; milling is inherently intermittent, so climb milling is not categorically unsuitable for interrupted cutting.
Advantages Of Conventional Milling
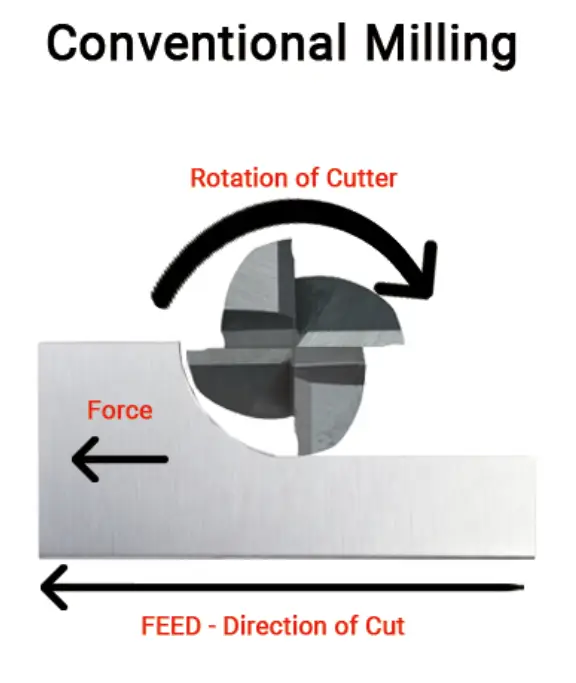
Conventional milling may be appropriate where machine or stock conditions favour it. It does not make an insecure or poorly prepared setup acceptable.
Reduced Risk of Backlash-Related Self-Feeding
Conventional milling may reduce the tendency for the cutter to pull the table forward through backlash. It does not remove mechanical wear or make a worn machine automatically safe; inspect and maintain the machine as required.
Consider Surface Condition and Tool Material
Surface scale, variable allowance, and cutting-tool material can affect the preferred direction. Do not choose conventional milling solely because the workpiece is hard; check application guidance for the specific material and cutter.
Greater Control
Force direction can influence deflection, but the result depends on geometry and support. Conventional milling does not compensate for setup errors, and roughing still requires controlled stock removal.
Stable On Light Machines
A Bridgeport or another manual mill should be operated according to its condition and instructions. A lightweight machine is not automatically more stable in conventional milling, and CNC machines also require appropriate rigidity and workholding.
Disadvantages Of Conventional Milling
Conventional milling can present wear and finish disadvantages in some applications. Evaluate these against machine and workpiece requirements rather than assuming a fixed penalty.
Excessive Tool Wear
Entry rubbing can increase friction and wear in conventional milling. The resulting temperature and tool life depend on cutting conditions; heat is not confined entirely to the tool.
Poor Surface Finish
Deflection or chip recutting can impair surface finish. Conventional milling does not inevitably require extra finishing; inspect the result against the specified surface requirement.
Work Hardening
Rubbing can contribute to work hardening in susceptible alloys. Avoid inadequate chip thickness and unsuitable cutting data; the effect depends on alloy and process rather than the milling direction alone.
Higher Cutting Forces
Some conventional-milling arrangements produce a lifting tendency. Design workholding for the actual force components without distorting the part; additional clamping or setup time is not inevitable.
Major Differences Between Climb Milling And Conventional Milling
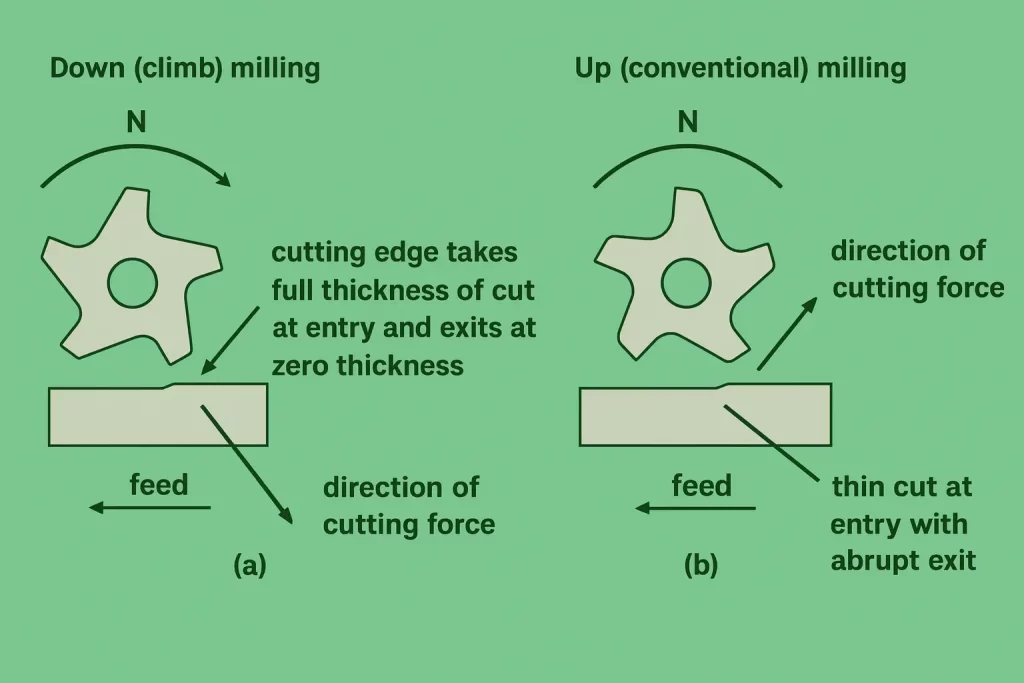
The cutting direction changes everything: chip formation, forces, finish, tool life.
Chip Formation Pattern
In peripheral milling, climb cutting generally forms a thick-to-thin chip and conventional cutting a thin-to-thick chip. Chip formation is important, but geometry, engagement, and cutting data also determine forces, temperature, and finish.
Cutting Force Direction
The familiar downward-versus-upward force description applies to particular peripheral-milling orientations. Do not transfer it unchanged to every vertical end-milling or face-milling setup; assess axial and radial forces for the actual tool.
Tool Engagement Mechanics
Entry and exit chip thickness affect edge loading. Select direction using the complete tool, stock condition, and machine setup; material hardness and rigidity alone do not describe every engagement condition.
What factors should you consider when choosing between Climb and Conventional Milling?
Your machine decides first. After that, the material decides. Finally, finish requirements matter.
Machine Tool Capabilities
Inspect backlash and feed-system condition using the machine manufacturer’s measurement procedure. A hand-wiggle test, ballscrews, software compensation, or backlash eliminators alone do not establish that the complete setup is suitable for climb milling.
Material Properties
Consider alloy, hardness, surface scale, and tool grade together. Avoid a universal rule of climb milling for soft materials and conventional milling for hard materials; choose from application guidance and verified results.
Surface Finish Requirements
Climb milling is often useful for finishing where the setup permits it. Neither a mirror finish nor improvement on every finishing pass is guaranteed; verify surface quality against the drawing.
Workpiece Stability
Select direction and toolpath for the component’s stiffness and support. Part weight alone does not determine the method, and thin walls may deflect under either radial or axial cutting forces.
Cut Depth And Width
Radial engagement changes chip thickness and loading. In full-width slotting, opposite sides of the cutter involve climb and conventional engagement; it is not simply a choice between two equivalent modes.
When To Use Climb Milling
Consider climb milling when the machine feed system, workholding, and cutting tool are suitable. It is often a useful starting choice for CNC production and finishing, but software backlash compensation alone is not approval for the operation.
When To Use Conventional Milling
Consider conventional milling where the machine’s operating instructions or stock condition favour it. Verify the tool and parameters instead of relying only on whether the machine is manual or the material is hard.
Correct inadequate rigidity or workholding before cutting. Changing milling direction does not make an unstable setup acceptable.
Best Practices For Climb Milling And Conventional Milling
After establishing a suitable setup, compare permitted strategies in controlled trials. Measure finish and monitor wear at intervals appropriate to the operation; a fixed 20-part interval is not universal.
Use sharp tools regardless of the method. Dull tools amplify every problem. Monitor cutting sounds. A change in tone means something changed. Stop and check.
Use secure workholding designed for the actual cutting forces. Avoid both movement and excessive clamping distortion.
Select the CNC coolant or dry-cutting strategy specified for the tool and material. Fluid is not compulsory for every milling operation, and intermittent cooling can be detrimental in some conditions.
The Bottom Line
Climb milling is commonly preferred when the setup permits, while conventional milling remains useful in particular conditions. Verify mechanical condition, tooling, workholding, and measured results; machine age alone does not decide the method.