










Minimizing Chatter and Vibration in CNC Turning: Effective Strategies and Inspection Steps
Learn how to optimize CNC turning operations by reducing chatter and vibration. Discover expert strategies like proper tool selection, parameter optimization, and workholding techniques. Explore essential inspection steps to identify and address problems, ensuring smoother machining processes and superior part quality.
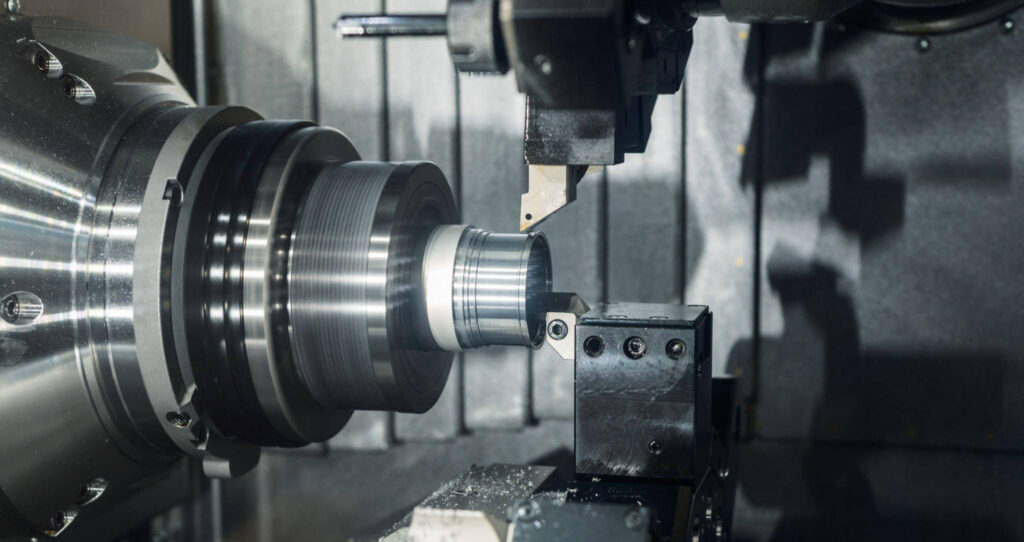
What Are Chatter and Vibration, and What Causes Them?
Chatter and vibration are unwelcome occurrences in CNC turning, characterized by undesired repetitive movements during machining. These phenomena can result in subpar surface finishes, diminished tool longevity, and decreased overall productivity. A comprehension of their origins and repercussions empowers manufacturers to proactively counteract or mitigate their impact.
Vibration can be forced by sources such as imbalance or interrupted engagement, while machining chatter is a self-excited instability of the cutting system, often involving regeneration of surface waviness. Tool and workpiece stiffness, damping, cutting geometry, and cutting conditions affect stability. Identify the source rather than treating every vibration as the same problem.
What is the Importance of Smooth CNC Turning and Effects of Chatter on Machining?
Smooth CNC turning holds significance beyond mere aesthetics; it profoundly influences the quality and utility of the end product. In the presence of chatter and vibration, machining precision dwindles, resulting in inaccuracies and irregularities within the workpiece. Consequently, components that fail to meet stipulated specifications materialize, driving up rejection rates and ultimately impacting a company’s financial bottom line.
The ramifications of chatter encompass several unfavorable outcomes, notably:
- Poor Surface Finish: Vibrations induce imperfections on the workpiece surface, leading to an undesirable finish.
- Reduced Tool Life: Chatter-derived forces hasten tool wear and breakage.
- Inaccuracies: Chatter-induced vibrations prompt deviations from intended dimensions and tolerances.
- Noise and Discomfort: Excessive chatter contributes to noise pollution in the workspace, adversely affecting operator comfort.
How to minimize Chatter & Vibration for Smooth CNC Turning
Minimizing chatter and vibration is crucial for achieving smooth CNC turning operations and obtaining high-quality machined parts. Here are some strategies to help you achieve this:
- Select Proper Cutting Tools:
Choose cutting geometry and grade for the material and setup. A smaller nose radius and a suitable positive geometry may reduce radial loading in a vibration-prone setup, but must still satisfy edge-strength, feed, depth-of-cut, and finish requirements. A larger nose radius is not automatically more stable.
Opt for tools with higher rigidity to withstand cutting forces and reduce tool deflection.
- Optimize Cutting Parameters:
Adjust spindle speed, feed per revolution, and depth of cut within the tool and machine limits using controlled trials. The direction of a useful speed change depends on the instability; reducing every parameter is not a universal remedy, and too little chip thickness can promote rubbing.
Use manufacturer-recommended cutting data as a starting point and make gradual adjustments.
- Use High-Quality Workholding:
Use suitable chuck jaws or fixtures and adequate support for the workpiece. Where appropriate, a tailstock or steady rest can support a slender part. Apply the specified clamping conditions without distorting thin walls; simply increasing clamping force does not guarantee stability.
- Check Machine Rigidity:
Use a rigid CNC lathe with minimal backlash and play in its components to prevent vibrations from being amplified.
- Implement Damping Techniques:
Use dampened cutting tools or tool holders designed to absorb vibrations and reduce chatter.
Consider using internal dampening systems in tools to mitigate vibrations.
- Apply Vibration Dampening Inserts:
Use a purpose-designed damped tool or holder installed according to its manufacturer’s instructions. Do not insert improvised rubber or polymer layers between the tool and holder, as this can reduce clamping rigidity and compromise tool retention.
- Utilize Adaptive Control Systems:
Where supported by the machine and control system, validated monitoring or adaptive-control functions may help detect instability and adjust operating conditions. They do not guarantee prevention of chatter or replace a sound mechanical setup.
The effectiveness of these systems depends on the sensors, control response, available adjustment functions, and the dynamics of the application; verify their performance under the intended cutting conditions.
- Use Smoother Tool Paths:
Opt for tool paths that minimize sudden changes in direction or engagement to reduce abrupt forces that can lead to vibrations.
- Avoid Excessive Overhang:
Keep unsupported tool overhang as short as practical while maintaining the required access and clearance. For boring bars, use a suitable diameter, specified clamping length, and any prescribed damping range. Measure overhang from the supporting clamp, not simply from the visible holder end.
- Inspect and Maintain Tools:
Regularly inspect cutting tools for signs of wear or damage that could contribute to vibration.
Replace worn tools promptly to maintain stable machining conditions.
- Consider Vibration Analysis:
Perform vibration analysis of the machining process to identify critical frequencies and make adjustments accordingly.
- Experiment and Fine-Tune:
CNC turning often requires experimentation to find the optimal combination of cutting parameters, tooling, and techniques that work best for a specific application.
- Employee Training:
Train operators and machinists to recognize the signs of chatter and vibrations and provide them with the knowledge to adjust parameters as needed.
What are the specific inspection steps to identify problems?
- Tool Inspection:
Examine the cutting tool for wear, chipping, or damage.
Ensure the tool’s geometry matches the machining requirements.
Check for proper tool clamping and seating in the tool holder.
- Workpiece Inspection:
Verify the workpiece material and dimensions match the machining specifications.
Check for any irregularities or imperfections on the workpiece surface.
- Cutting Parameters Review:
Evaluate the cutting speed, feed rate, and depth of cut used during machining.
Compare the parameters with recommended values for the material being machined.
- Workholding and Fixturing:
Inspect the work holding setup for secure clamping and accurate positioning.
Check for any signs of workpiece movement or vibration during machining.
- Machine Rigidity and Stability:
Assess the CNC lathe’s rigidity and stability by examining components for wear, backlash, or excessive play.
Ensure all machine components, including slides and bearings, are properly lubricated and maintained.
- Cutting Fluid Application:
Check coolant delivery and chip evacuation against the tool grade, material, and operation. Use the supplier’s recommended wet or dry strategy; coolant is not by itself a cure for a structurally unstable setup.
- Tool Path Evaluation:
Analyze the tool path for sudden changes in direction, sharp corners, or excessive engagement.
Opt for smoother tool paths that minimize abrupt changes.
- Vibration Analysis:
Use vibration sensors or monitoring systems to analyze vibrations during machining.
Identify critical frequencies where vibrations are most prominent.
- Surface Finish Inspection:
Examine the surface finish of machined parts for signs of poor finish, irregular patterns, or waviness.
- Operator Feedback:
Gather feedback from machinists and operators who have firsthand experience with the machining process.
Obtain insights into any observed chatter or vibration issues.
- Trial and Adjustment:
Conduct controlled trials by making incremental adjustments to cutting parameters, tooling, or fixturing.
Observe how changes affect chatter and vibrations and document the outcomes.
- Documentation and Analysis:
Maintain records of inspection results, adjustments made, and their effects on machining performance.
Analyze the collected data to identify patterns and trends related to chatter and vibrations.
- Continuous Improvement:
Use the insights gained from inspection and analysis to implement ongoing improvements in the machining process.
Conclusion
By following these inspection steps and implementing improvements based on your findings, you can effectively minimize chatter and vibrations during CNC turning processes, resulting in smoother operations and improved part quality.
Tagged tech news