










What is Center Drill? Definition, Types, and Applications
In CNC machining, starting a hole accurately requires suitable tooling and entry preparation. A center drill primarily produces a center hole for supporting a workpiece between centers. It should not automatically replace a spot drill or a specified pilot drill.
Contents
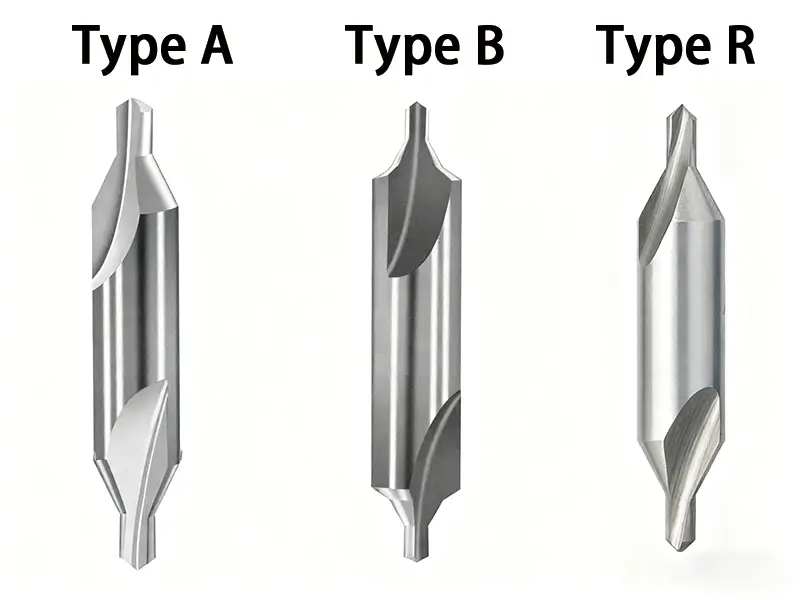
What is Center Drill?
A center drill is used in CNC machining to produce a small pilot portion and a seating form for a machine center. The center hole supports the workpiece during suitable turning or grinding operations. It does not clamp the part by itself, and is not automatically the correct starting hole for a larger drill.
Center drills have other applications as well, which we’ll discuss in the next section. Let’s take a look at the design of this tiny tool:
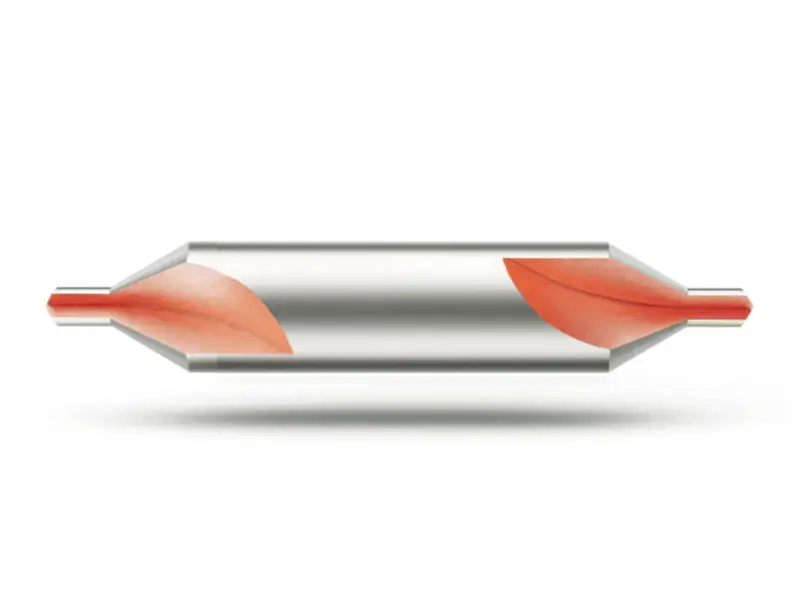
Pilot
The pilot is the small-diameter drilling portion ahead of the seating form. Its geometry depends on the tool design. It is vulnerable to damage if alignment, feed, or chip clearance is unsuitable.
Some twist drills need entry preparation, while other designs can start directly in suitable material. Follow the subsequent drill’s instructions rather than assuming a center-drilled hole is always needed.
Countersink
The wider cutting portion forms the seating surface in the workpiece. The machine center contacts that finished surface; the center drill itself is removed before the supported machining operation.
Types of Center Drill
Center drills come in various shapes and sizes. They can be classified based on the material type and geometry.
Based on Material
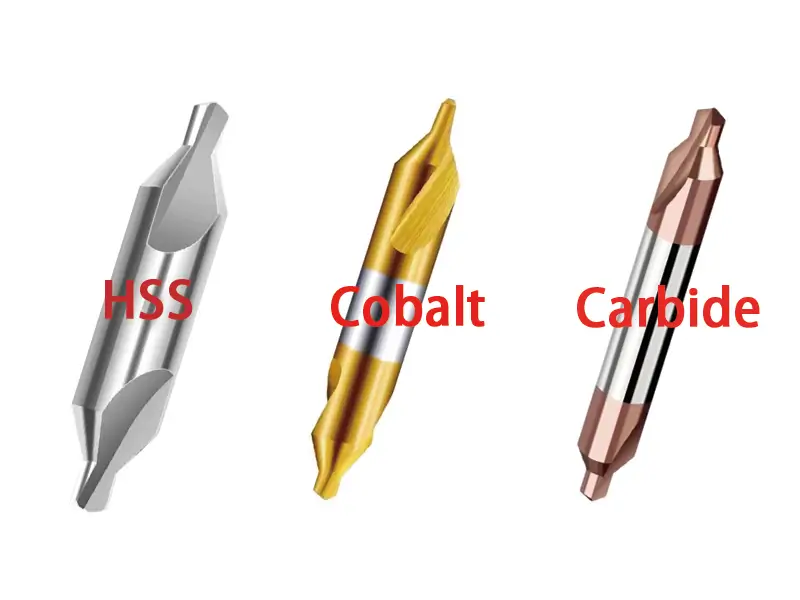
HSS
High-speed steel center drills are available for a range of materials. Suitability depends on grade, geometry, workpiece hardness, and cutting conditions; HSS does not inevitably fail on every harder material.
Cobalt
Cobalt center drills are basically HSS drills with a higher percentage of cobalt. Cobalt increases the wear and heat resistance of center drills.
Carbide
A carbide center drill can offer wear resistance in a suitably rigid and accurate setup. Speed, feed, tool life, and precision depend on the application; carbide alone does not guarantee maximum accuracy or longer life.
Based on Geometry
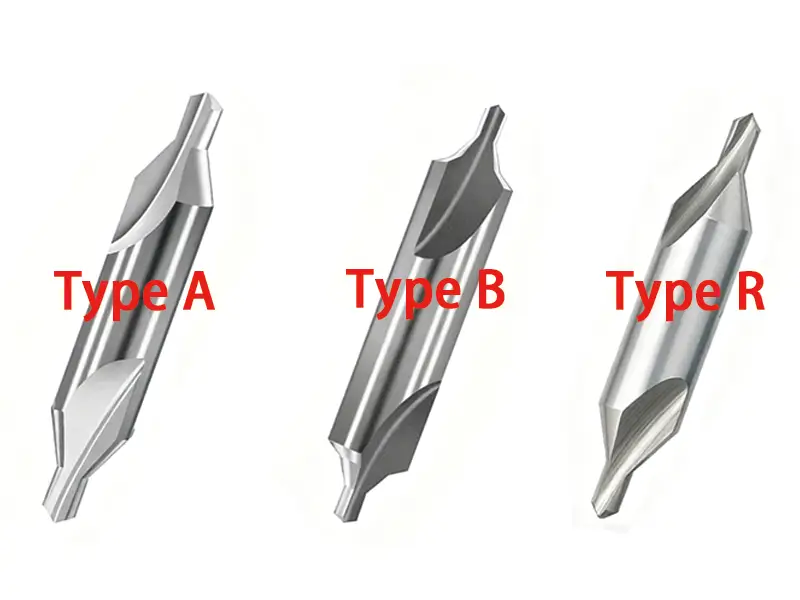
Type A
Type A is the most basic type of center drill with a 60° conical angle. It follows the DIN 333-A standard. This type of center drill is used for creating center holes or spotting holes in shafts.
Type B
Type B center drill has 2 chamfers for enhanced performance. It is based on the DIN 333-B standard. This center drill has a 60° countersink and 120° protective chamfer. This 120° chamfer protects the 60° cone from being damaged during the application.
Type R
As compared to type A and type B, type R has a very different geometry. It features a radius instead of a chamfer. It has a pilot tip followed by a curved section. This advanced design provides various advantages in machining.
Uses of Center Drill in Machining
In the machining industry, precision is non-negotiable. You need to meet the requirements of tight tolerances. And sometimes, achieving those can become difficult. Center drilling is a small step that can save you a lot of time and rework. Here, we have included some of the common uses of center drilling in the machining process:
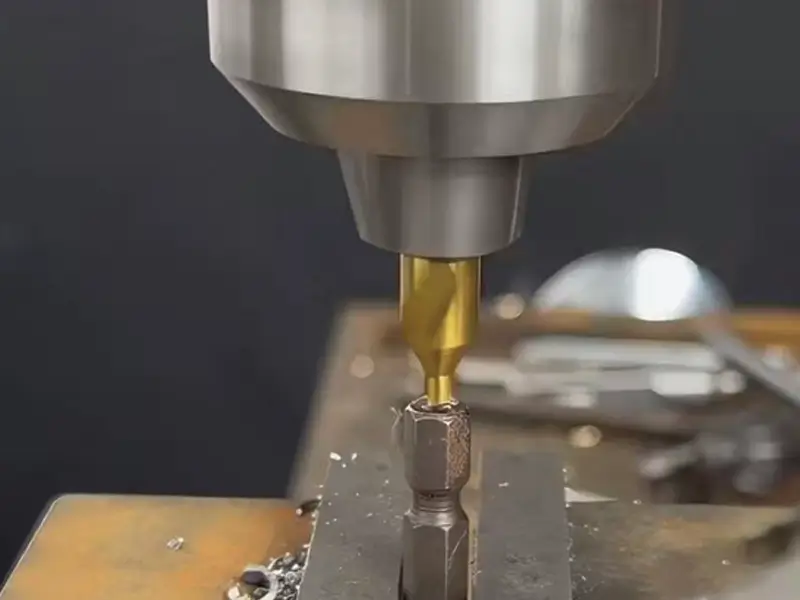
Creating a Center For Long Parts on a Lathe
Long workpieces may require centers and additional supports appropriate to their length and stiffness. Where specified, center holes with a 60° seating form support the workpiece. Correct alignment, seating, drive, and loading remain necessary; the holes do not guarantee freedom from vibration or slipping.
Drilling Pilot Holes
For deep holes drilling, use the entry preparation specified for the chosen drill. A center-drilled hole is not interchangeable with a controlled pilot bore and does not guarantee a smooth and polished surface.
Chamfering
Chamfering can remove a sharp edge and support assembly, but the required angle and size come from the drawing. Use a suitable chamfering tool; a center drill is not a universal substitute. Deburring reduces a hazard but does not guarantee injury prevention.
Step-by-Step: How to Use a Center Drill
Let’s go through the steps of using a center drill:
- Select the center-hole form and size from the drawing, support requirements, material, and machining process. Workpiece diameter alone is insufficient to select the center drill.
- Secure the workpiece and tool with suitable workholding and alignment. A three-jaw chuck holder is one possible arrangement, not a universal requirement; check grip and runout before cutting.
- Depending on the material of the workpiece and the diameter of the center drill that you are using, adjust the rotational speed.
- With guarding and setup checks complete, use the specified cutting conditions and feed to the required depth. Follow the machine’s procedure rather than approaching a rotating tool by hand.
- Stop the spindle completely before inspection. Check the center-hole form, size, surface condition, and seating requirements before proceeding.
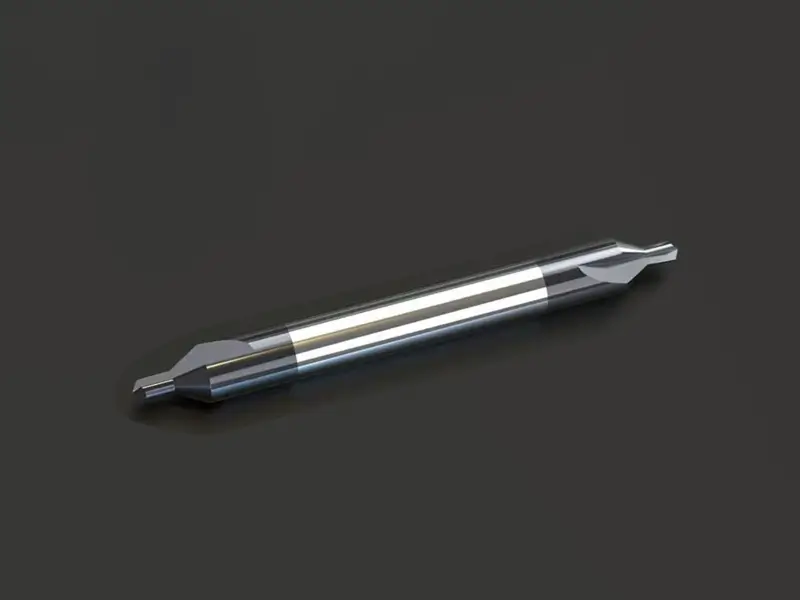
Choosing the Right Type Of Center Drill
Before choosing the type of center drill (A, B, R), consider your requirements. Whether you need high precision, heavy grinding, or some everyday work. Here’s when you should select each type:
Type A
Type A produces a plain center-hole seating form. It can be used for precision work when the drawing and process specify it. Selection should depend on the required center-hole design rather than a blanket prohibition on precision-critical components.
Type B
Type B includes a protective outer chamfer around the center-hole seating surface. This protects the seating edge, not the tool’s pilot point. Use it when the specified center-hole design requires that protection.
Type R
Type R uses a radiused seating form. Select it according to the required center-hole geometry and supporting center arrangement; it is not automatically the best choice for hard materials, heavy grinding, or maximum tool life.
Conclusion
Center drills produce center-hole forms for supported machining. Types A, B, and R are common forms rather than the only center-drill designs. Match the tool to the specified geometry and process. Contact Sundi for PCD, PCBN, and carbide cutting tools.